Blog

How to Test an HDMI Cable Before Accepting a Bulk Lot: Pinout, TMDS and 4K Checks

A bulk lot of HDMI cables can look perfect on arrival and still fail in the equipment rack: no picture at 4K, sparkles during motion, or a signal that drops whenever someone touches the cable. The eye test at the loading dock catches none of that. What catches it is a fixed acceptance routine: continuity against the 19-pin map, a full-link test at the resolution you actually ship for, and a purchase order that says in advance what counts as a failed lot. This article lays out how to test HDMI cable assemblies at acceptance, in the order we recommend running it, with the pass criteria for each step.

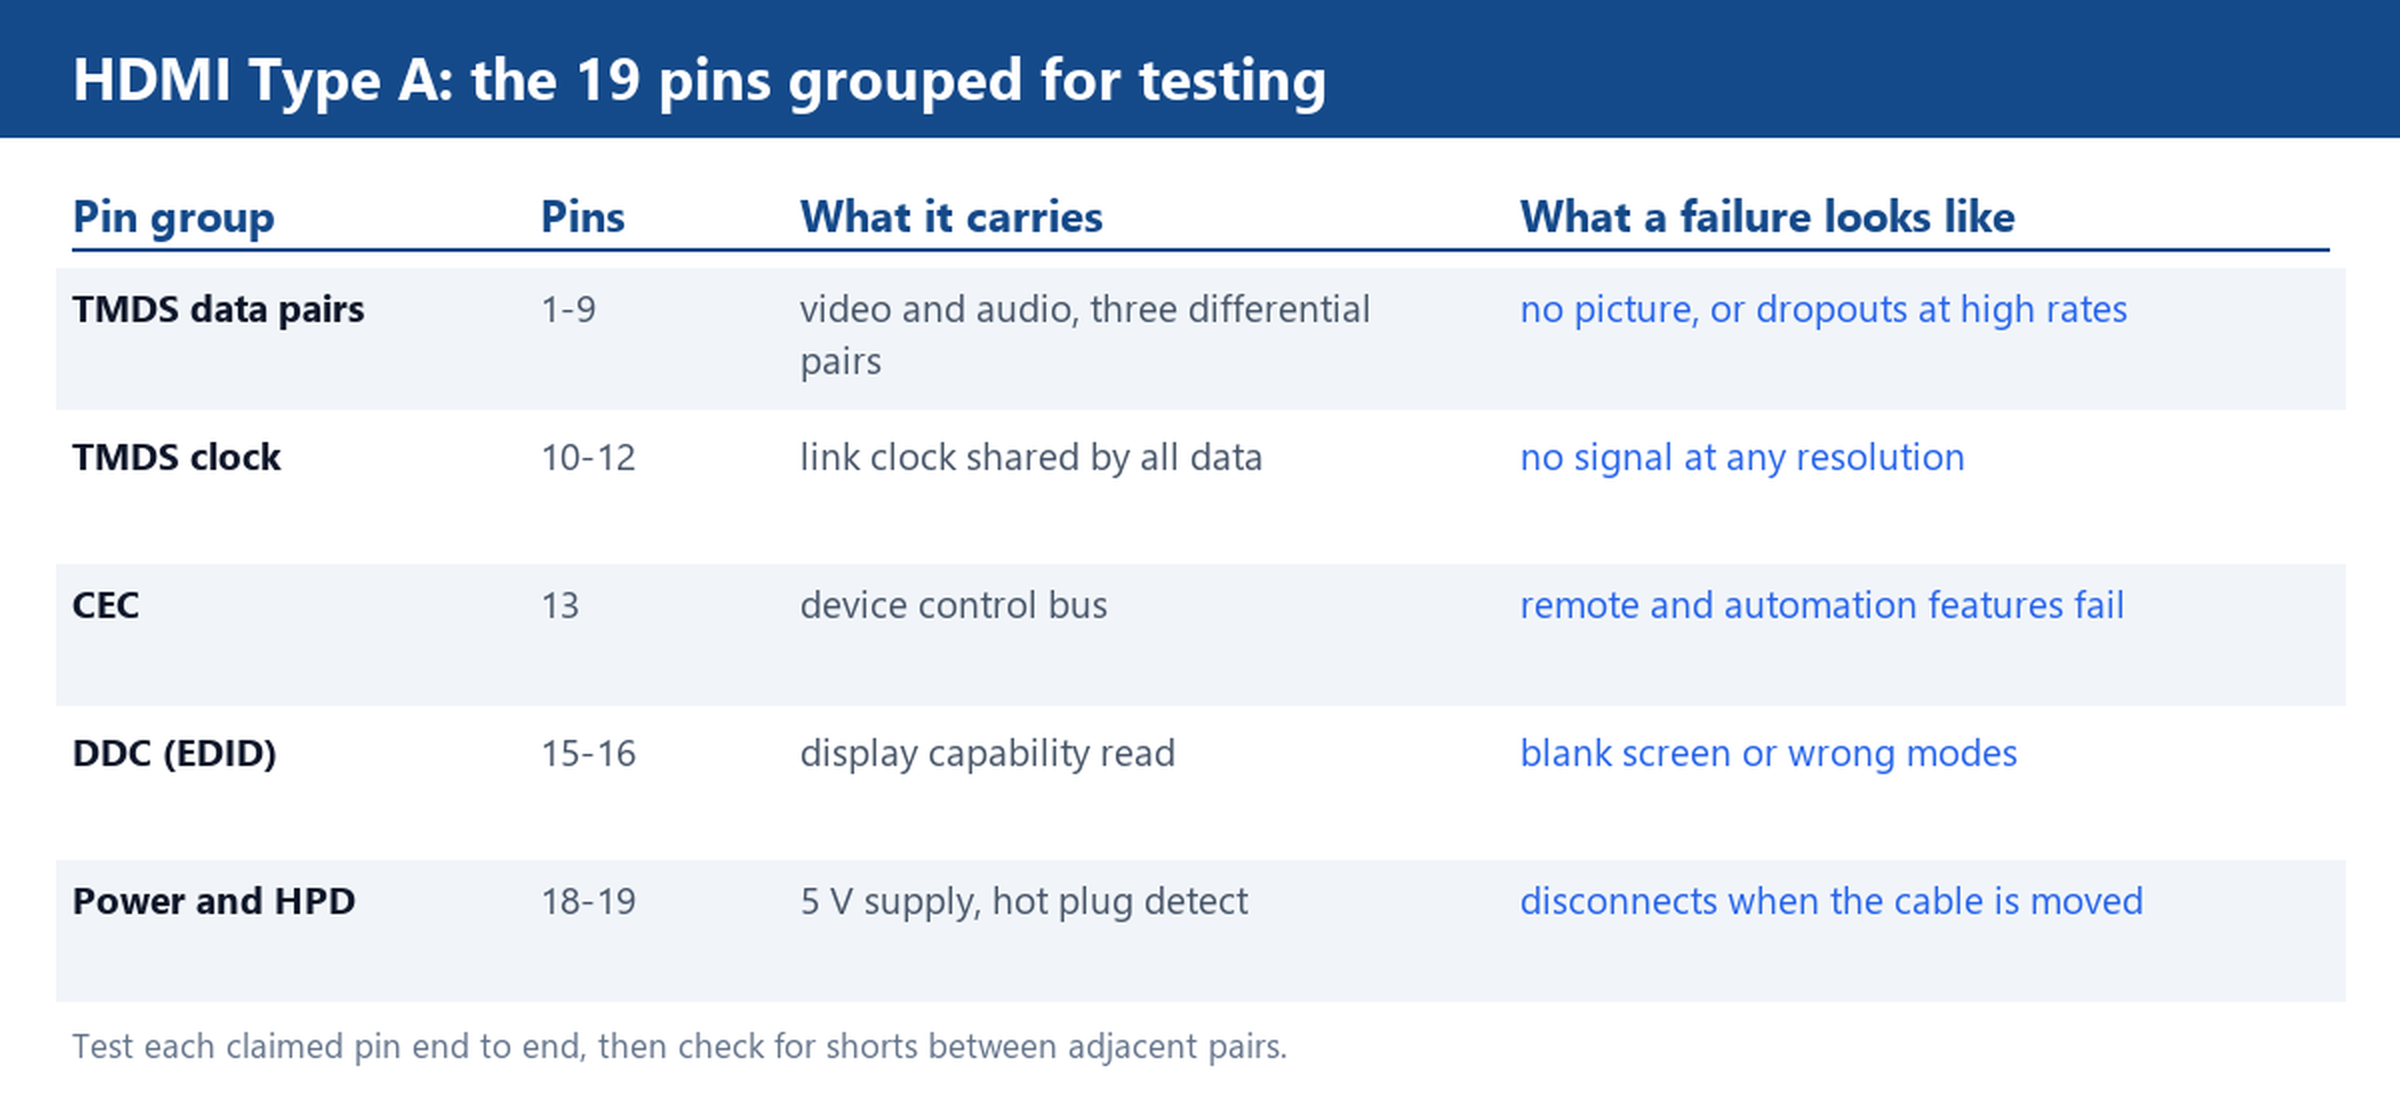
Table grouping the 19 HDMI Type A pins for testing: TMDS data pairs on pins 1 to 9, clock on 10 to 12, CEC on 13, DDC EDID lines on 15 and 16, and 5 volt supply plus hot plug detect on 18 and 19, with the failure each group causes
Each pin group has a signature failure, which makes the bench test fast to interpret.

Prefer watching? The full walkthrough is below — pinout, TMDS pairs and the 4K check, in the same order as this article.

What a cheap cable tester can tell you, and what it cannot

An inexpensive pin tester is the right first filter. Wired to two sockets, it reports continuity pin by pin and flags open circuits, shorts between adjacent conductors and crossed pins. On a lot of a few hundred cables this removes the dead units in minutes and costs almost nothing per check.

The same tester cannot certify the link. It does not drive a real TMDS signal at multi-gigabit rates, it does not measure shield coverage, and it says nothing about how the assembly behaves when the cable is flexed or the plug is wobbled. Treat it as a filter, not as an acceptance certificate. Everything after this step exists to catch what the tester cannot see.

Pin-by-pin continuity: TMDS pairs, clock, control and power

The 19 pins of an HDMI Type A plug divide into clean groups, and each group has a signature failure. The three TMDS data pairs sit on pins 1 to 9 and carry video and audio as three differential pairs; a break in any pair means no picture or heavy dropouts, and a short between adjacent pins often shows up only at high data rates. The TMDS clock pair on pins 10 to 12 carries the shared link clock; if it is open there is no signal at any resolution, which is actually a useful signature because it is easy to reproduce. Pin 13 carries CEC, the control bus behind remote and automation features. Pins 15 and 16 are the DDC lines the source uses to read EDID from the display; a broken DDC line gives a blank screen or a device that only offers wrong modes. Pin 18 supplies 5 V and pin 19 is hot plug detect; when HPD is intermittent the display disconnects exactly when the cable is moved.

Probe each claimed pin end to end with the meter in continuity mode and expect a resistance near an ohm or less, then check for shorts between adjacent pins. On a plug-moulded assembly, wiggle the cable gently at the plug while probing; a reading that flickers marks a broken conductor inside the mould, which no static test reveals.
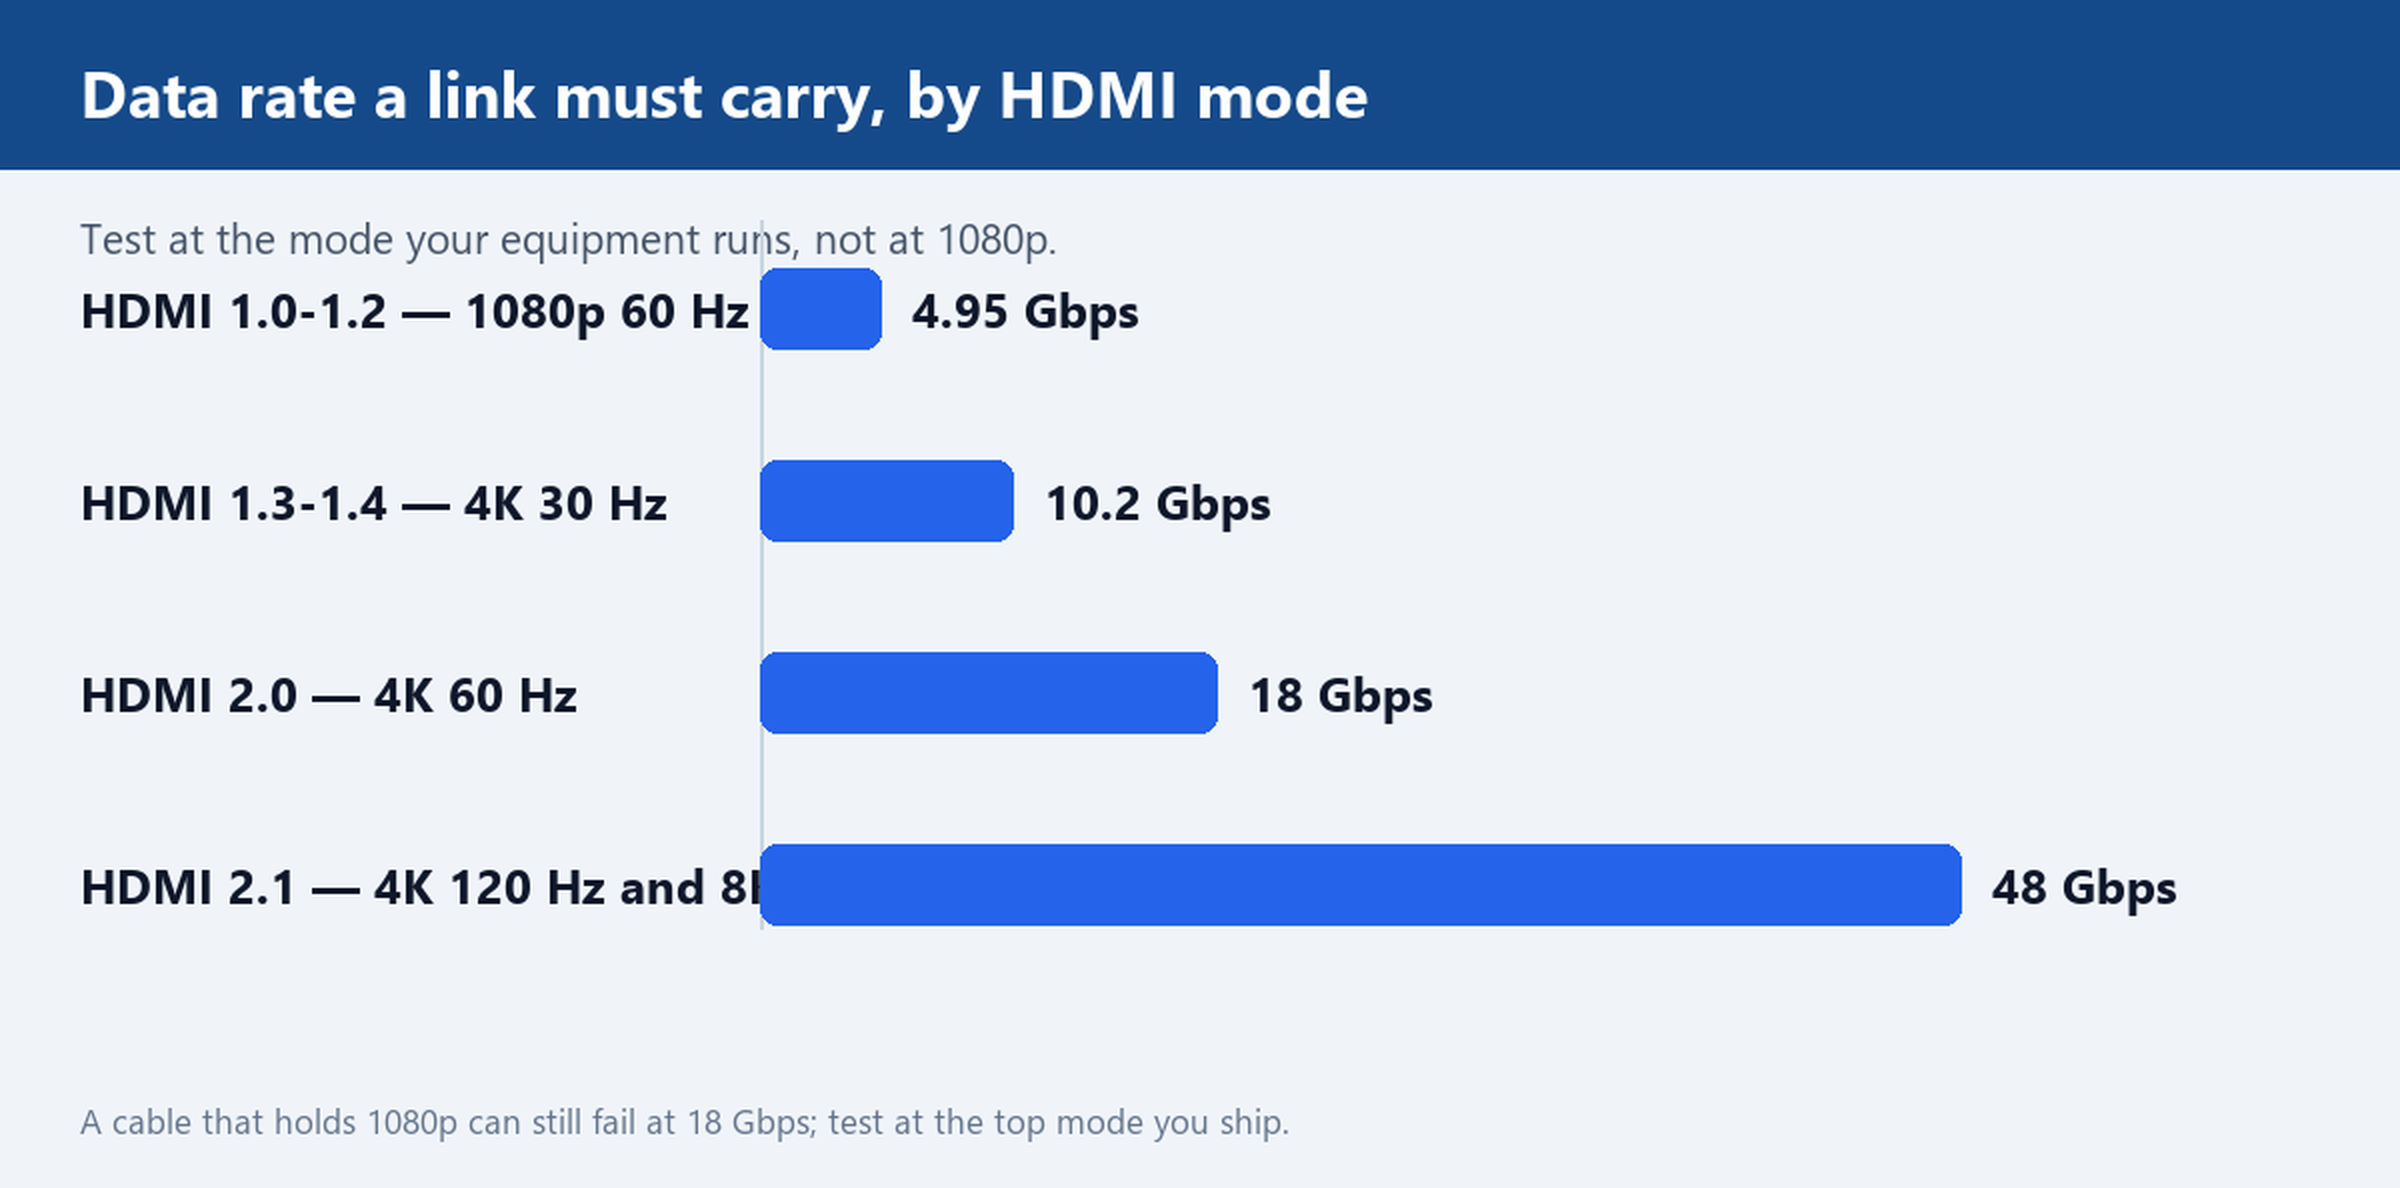
Bar chart of HDMI data rates: 4.95 Gbps for 1080p at 60 Hz, 10.2 Gbps for 4K at 30 Hz, 18 Gbps for 4K at 60 Hz and 48 Gbps for 4K at 120 Hz and 8K
Continuity can pass at 1080p and the same cable can fail at 18 Gbps.

Testing at the resolution you actually run, not at 1080p

Continuity proves the wires exist; only a live link proves the cable holds the data rate. The rates are not close together: 1080p at 60 Hz fits in the 4.95 Gbps class of early HDMI, 4K at 30 Hz fits in the 10.2 Gbps class, 4K at 60 Hz with full colour needs the 18 Gbps of HDMI 2.0, and 4K at 120 Hz or 8K needs 48 Gbps. A cable that plays 1080p for hours can fail at 18 Gbps in the first minute.

So test on the source and display combination you actually ship with, set to the top mode the product claims. The 4K HDMI 2.0 Braided Flat Cable, Gold Plated, for example, should be sampled against a source and display both locked to 4K at 60 Hz. Watch for the classic symptoms of a marginal link at rate: single-pixel sparkles, short blackouts during motion, or a handshake that needs several replug attempts. Let the link run for a defined soak period, ten to fifteen minutes is enough for most faults to surface, and record the mode used. The same rule applies to converter builds such as the USB-C to HDMI 4K 60Hz Cable, 1.8 m, where the whole assembly, not just the HDMI plug, has to hold the mode.

Failures that still pass a continuity test

Four failures pass a static bench and reject themselves only in service:

  • Intermittent contact under flex. A conductor cracked inside the mould reads fine at rest and drops when the cable bends. Flex the cable through its working radius during the live test.
  • Damaged shield. Continuity on every pin tells you nothing about braid coverage or a torn foil. Run the live link next to a known interference source; a failing shield shows as sparkles or audio ticks that a clean bench hides.
  • Wrong internal pinout at the plug. A crimp that lands a pair on the wrong blades still gives continuity, but swaps signal groups and fails at rate. The pin-map test in the previous section catches this only if you label which blade lands on which conductor end.
  • Connector fit. A plug that wobbles in the socket works on the bench and disconnects in the rack. Check retention by feel on every sampled unit, with the weight of the cable hanging on the plug.

What to write into the PO and the inspection checklist

Acceptance is enforceable only when the criteria are written before the lot ships. Three clauses do most of the work:

  • Test scope. Hundred percent pin continuity on every unit in the lot, plus a live-link soak at the rated mode on a stated sample per batch, with the mode and duration named.
  • Pass criteria. Continuity near an ohm or less per pin, no shorts between adjacent conductors, and a soak with no sparkles, dropouts or replug events.
  • Rejection rule. Any failure in the sample sends the batch back for retest of the full lot, and the retest record ships with the replacement.

Where the cable is custom in length or jacket, fold the same clauses into the custom sheet before tooling; the Customize Cable page lists what such a sheet should carry. For the products themselves, start from the HDMI Cables and HDMI 2.0 Cables categories, and the Audio & Video Cables category for the wider family. The Factory page covers line-side QC and How to order explains the sampling and confirmation sequence step by step.

Send your resolution and length requirement, and we will ship a sample HDMI cable with the test result recorded on the same production batch. A sample that arrives with its own test record is the fastest way to make the acceptance routine above a formality rather than a fight.

Short on time? The 76-second version covers the same three checks.
Read more...

USB-C E-Marker: Why a 5A Cable Needs the Chip and a 60 W Cable May Not

If you order a USB-C cable rated for 5 A, the cable must carry an e-marker chip inside one of the plugs. That chip is what tells the charger the cable is allowed to pull 5 A and reach 100 W; without it, any Type-C source caps the current at 3 A no matter how thick the copper is. A cable built for 60 W, which is 3 A at 20 V, can be perfectly correct without a chip. The buying risk is not the chip itself but the gap between sample and bulk lot: the sample carries the chip, the production run ships without it, and every end user notices slow charging within a week. This article sets out where the chip requirement sits, why the copper alone decides nothing, and the checks that keep a bulk order honest.

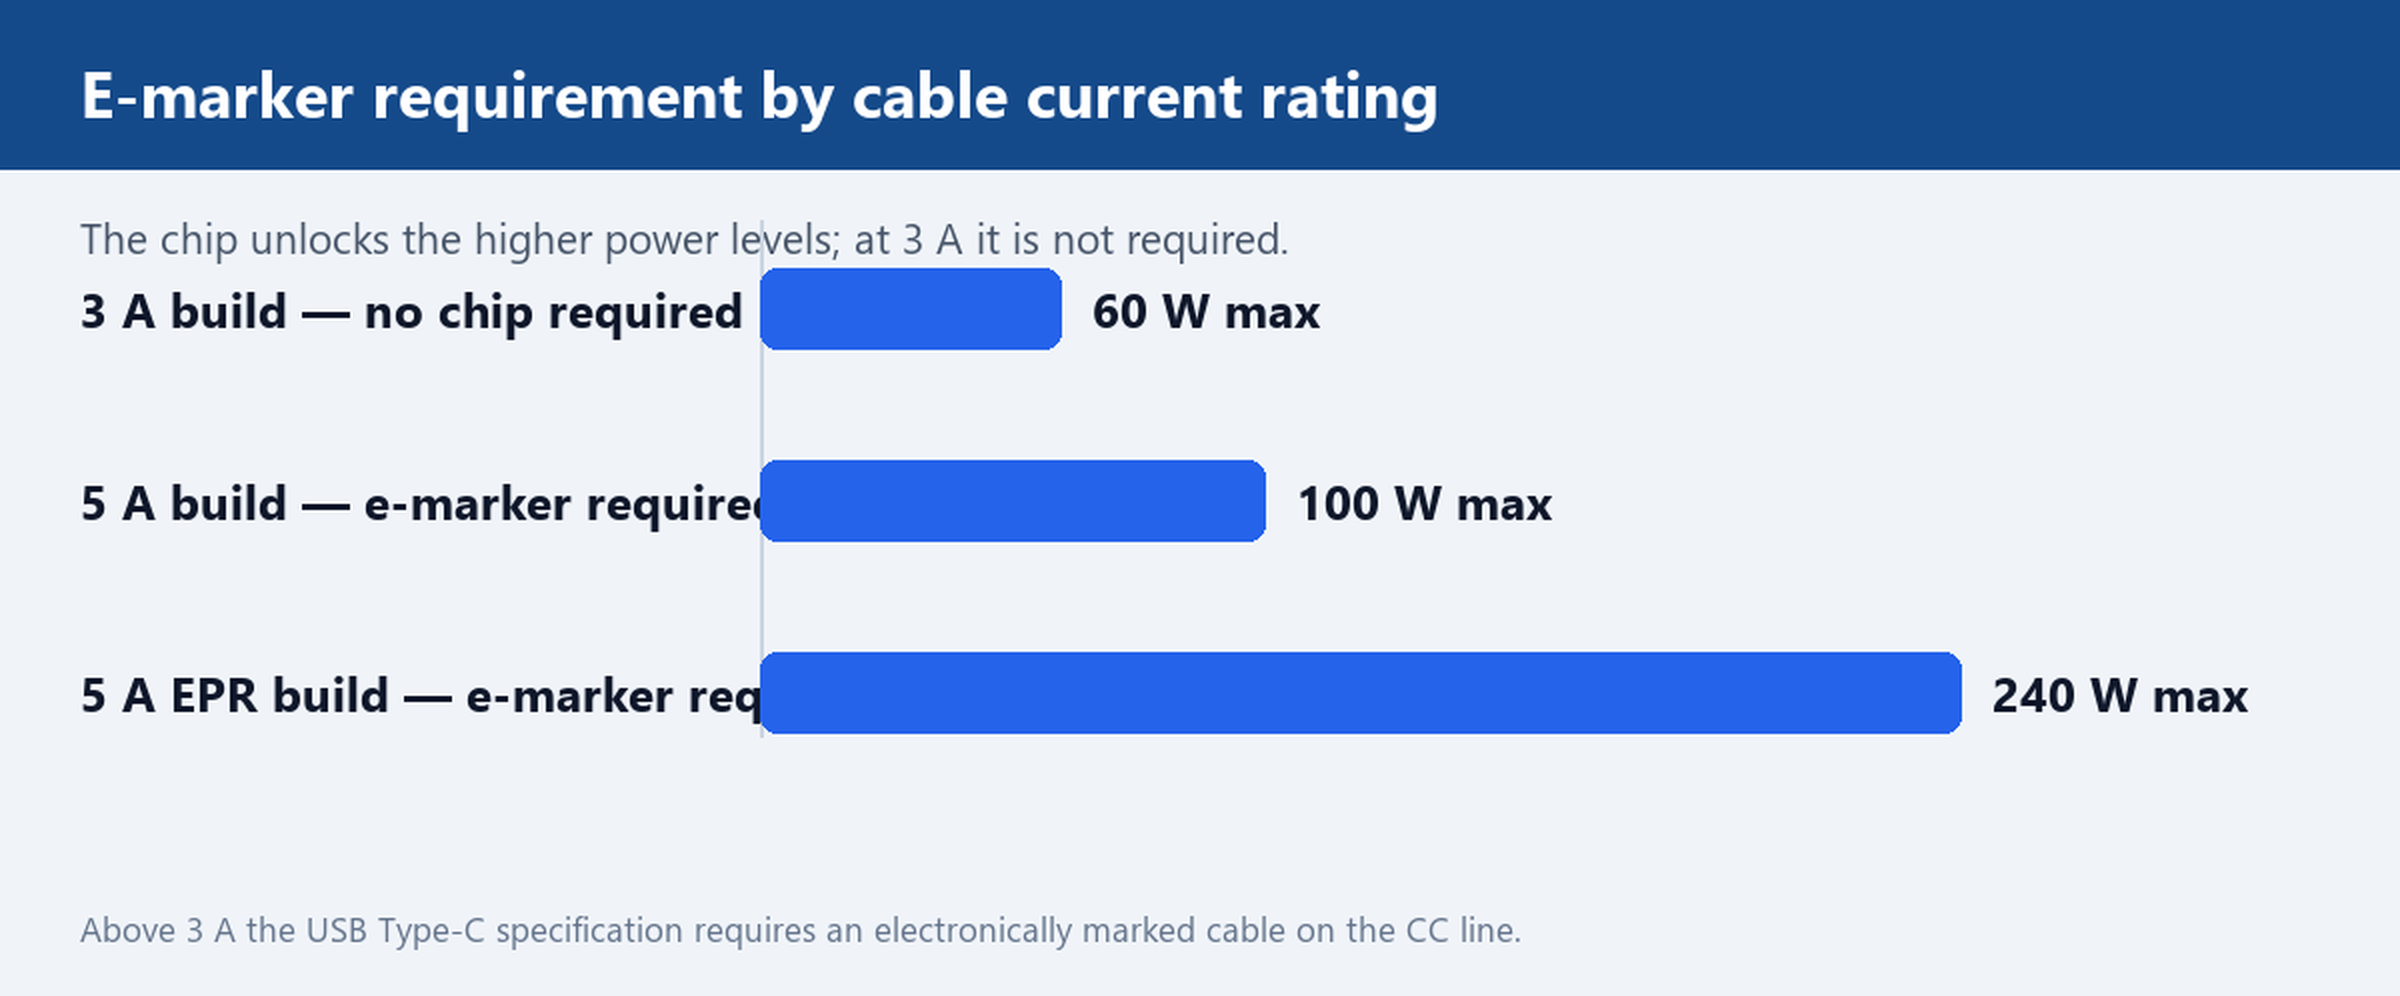
Bar chart comparing USB-C cable power ceilings: a 3 ampere cable reaches 60 watts with no e-marker, a 5 ampere e-marked cable reaches 100 watts and an EPR e-marked cable reaches 240 watts
Above 3 A the Type-C spec asks for the chip; below it the copper can work alone.

What the e-marker chip does

A USB-C e-marker is a small integrated circuit embedded in one plug mould and connected to the CC line. Every Type-C to Type-C cable already carries passive resistors on that line, which announce that a functioning cable is present. The marker is extra silicon that answers questions. When a charger and a device connect, the source talks to the cable over the CC wire and asks what the cable can carry. A marked cable replies with its rated current and its supported voltage ranges. An unmarked cable replies with nothing, and the source assumes the safe default of 3 A. The negotiation then stops there, regardless of the conductor size inside the jacket.

The marker stores plain electrical facts: the maximum current the cable is rated for, whether it supports the higher voltage ranges used above 100 W, and in many builds the cable length. It holds no firmware and cannot be updated from the charger side. That is why the chip question has to be settled at the factory, not at the support desk.

Where the line sits: 5 A cables carry the chip, 60 W builds often do not

The rule in the USB Type-C specification is short: a cable that carries more than 3 A must be electronically marked. Below 3 A the marker is optional, and most factories skip it because a chip adds cost with no benefit at 60 W. Two builds from the USB Type-C Cables range show the split. The USB-C to USB-C 60 W Cable, Gold Plated, 3 m is built for 20 V at 3 A, so it ships without a marker on purpose. The 5A USB-C to USB-A SuperCharge Cable, Braided is built for 5 A-class current on the power conductors; on a Type-C to Type-C link that rating is only unlocked by a marked cable, while on a USB-A charger the current flows under the older default rules and the wire gauge does the work.

In practice, buyers should treat the marker as a rating question, not a quality question. A 60 W cable without a chip is correct engineering. A 100 W cable without a chip is not a 100 W cable at all; it is a 60 W cable with thicker copper and a print that promises more than the negotiation can deliver.

Why a missing chip caps charging even when the copper is thick enough

The failure mode is quiet. The cable works, the laptop charges, nothing overheats. But a 100 W laptop on a 20 V charger pulls only 3 A, so it charges at 60 W, roughly half the rate the buyer paid for. Phone charging slows down the same way. Because the cap comes from the negotiation table, swapping the charger does not fix it and no device firmware update fixes it either. A practical fix is a cable whose marker reports 5 A; everything else leaves the cap in place.

This is also why the fault clusters in bulk lots rather than in samples. The factory ran the sample line with marked plugs and the mass production line with cheaper unmarked ones, or the plug supplier changed between runs. The copper did not change, the print on the jacket did not change, and the shortfall only shows up when a user plugs into a high-power charger.

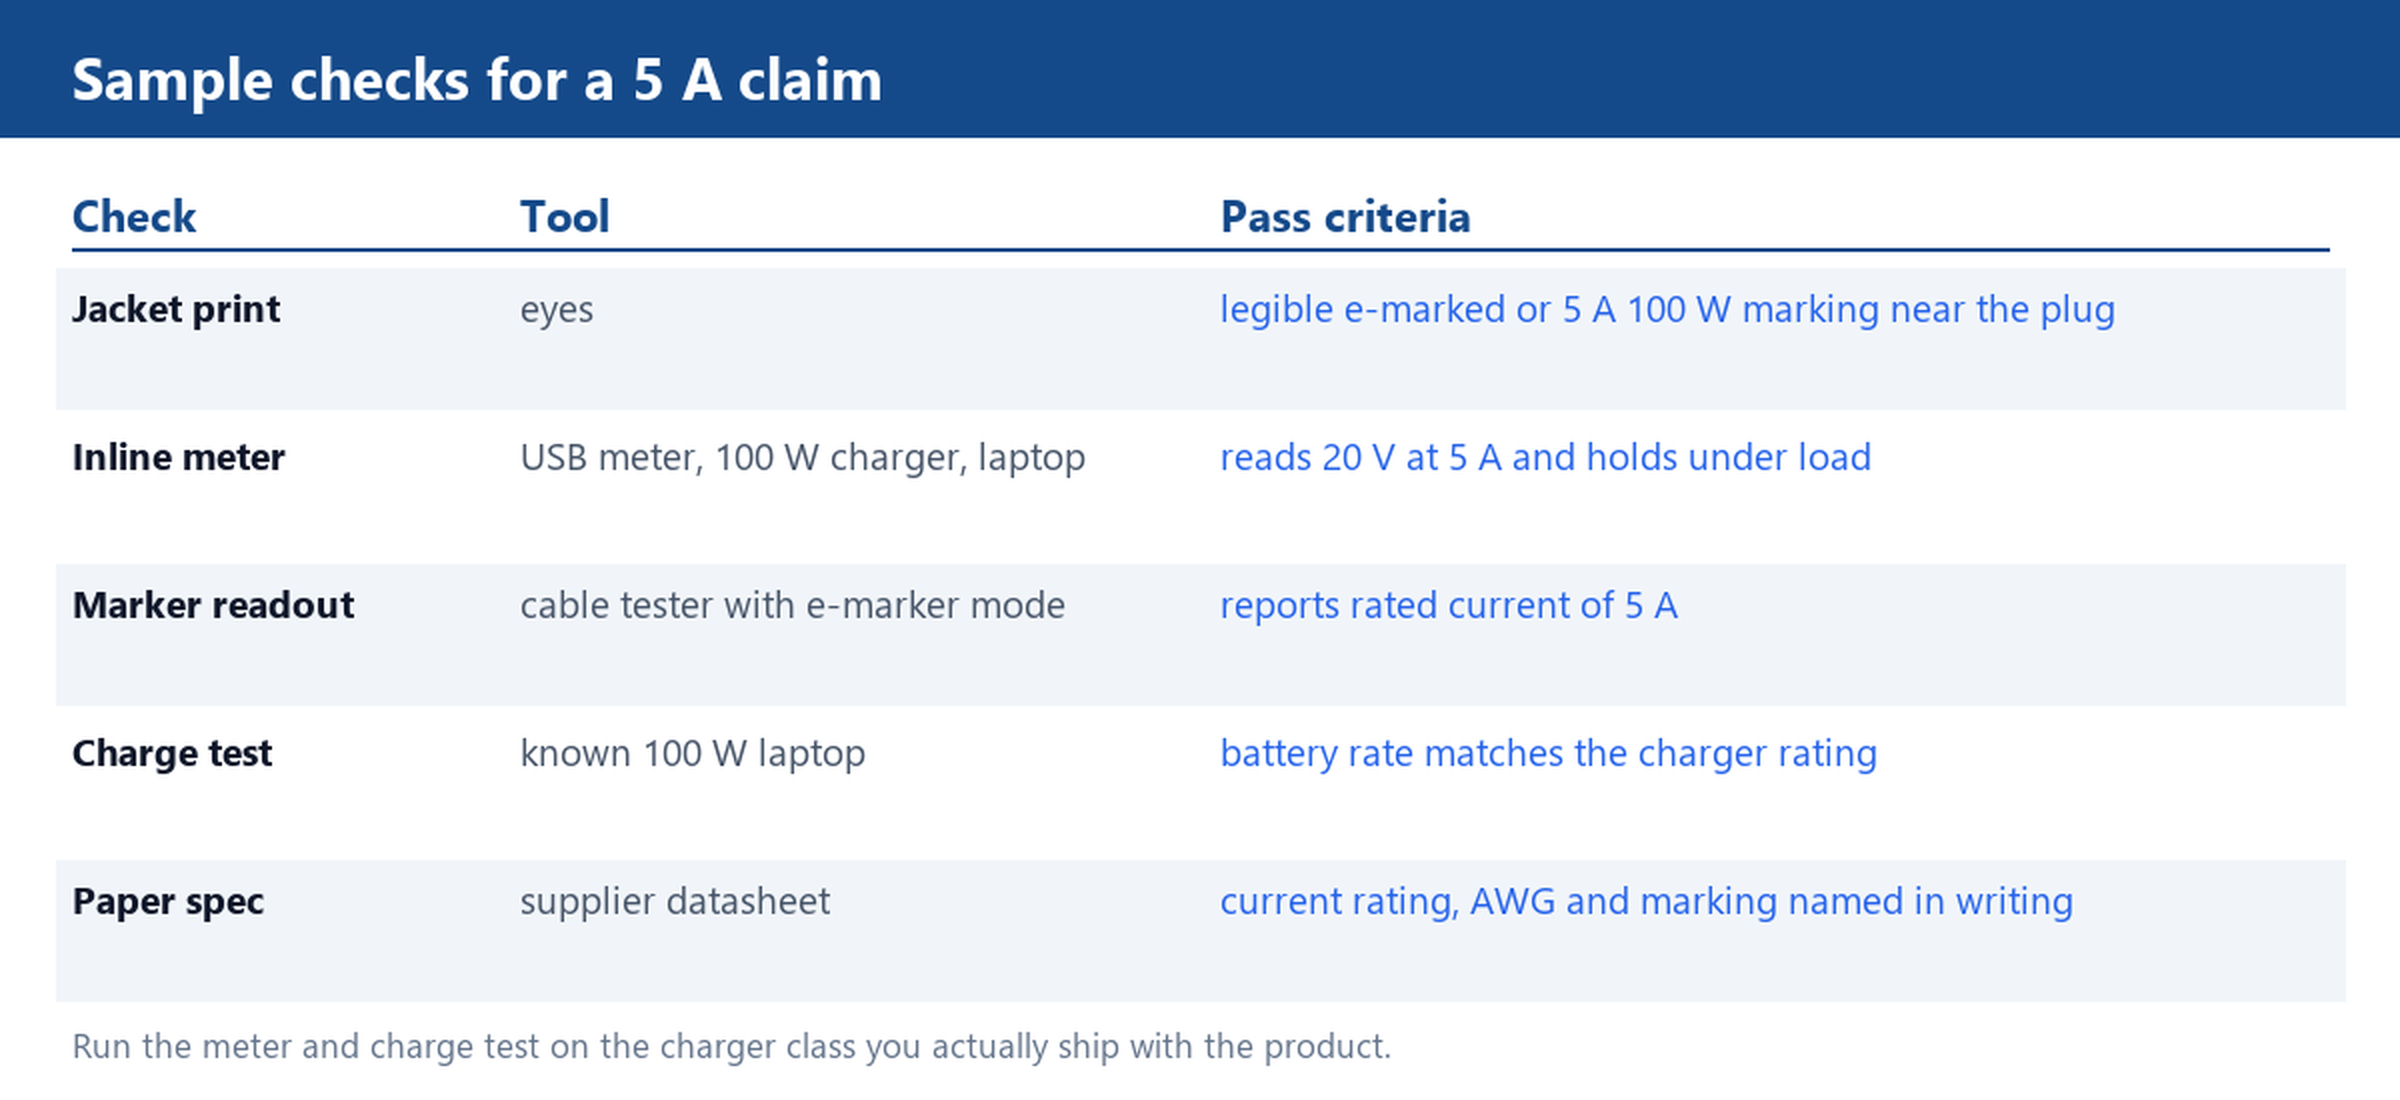
Table of five sample checks for a 5 ampere USB-C cable claim: jacket print, inline USB meter reading 20 volts at 5 amps, cable tester marker readout, charge test on a 100 watt laptop and written spec confirmation
Run the meter check on the charger class the product will actually ship with.

How to check a sample before the bulk order

Four checks, in order of cost:

  • Jacket and plug print. A marked cable usually carries an e-marked or 5 A print near the plug mould. Absence of print is not proof that the chip is missing, but a clear print at least tells you the factory tracked the rating.
  • Inline USB meter. Put a meter between a 100 W charger and a laptop that accepts 100 W. A marked 5 A cable negotiates 20 V at 5 A. An unmarked one sits at 20 V 3 A. Record both numbers.
  • Tester readout. Bench testers with an e-marker mode read the chip directly and display the rated current. This is the fastest check on a large sample table.
  • Charge test on a known device. Charge the same 100 W-class laptop on the original cable and on the sample, then compare the charge rate the operating system reports.

Run the meter and charge test on the charger class you actually sell into, not on whatever is on the bench. The Charger Cables category shows the pairings buyers ask for most, and the same logic applies: the test has to match the end use.

Specifying the rating in your PO

Wording decides whether a claim is enforceable. Ask for three lines in writing:

  • Electronically marked cable, rated 5 A at 20 V (100 W), stated on the datasheet and on the test report.
  • Power conductor gauge named explicitly, typically 20 to 21 AWG on 5 A builds and 22 to 24 AWG on 3 A builds, with longer runs at the thicker end of the range to hold voltage.
  • Marker readout recorded per production batch, not per sample only.

Where the cable is custom in length, colour, jacket or plug moulding, the same three lines belong in the custom spec sheet before tooling starts. The Customize Cable page shows what a spec sheet should carry, the Factory page covers line-side inspection, and How to order walks through the sampling and confirmation steps in sequence. For the full catalogue by family, start at the USB Cables category.

Ask for a 5A e-marked sample plus a written current rating before you place the bulk order, and keep the meter reading from that sample taped to the PO. The two together turn a slow-charge complaint from a warranty argument into a five-minute replacement conversation.

Read more...

How to Test a USB Cable Before It Fails: 5-Minute Checks Anyone Can Run

A failing USB cable usually looks like a failing device. The phone charges but will not sync, the drive disconnects during a large file, the port works with one cable and not another. Before replacing hardware, five minutes with a multimeter, a USB meter and two known-good devices will tell you whether the cable is at fault, and roughly which part of it.

None of the checks below need a lab. This is how to test USB cable assemblies and separates with a meter, two known-good devices, and a written record of what passed.

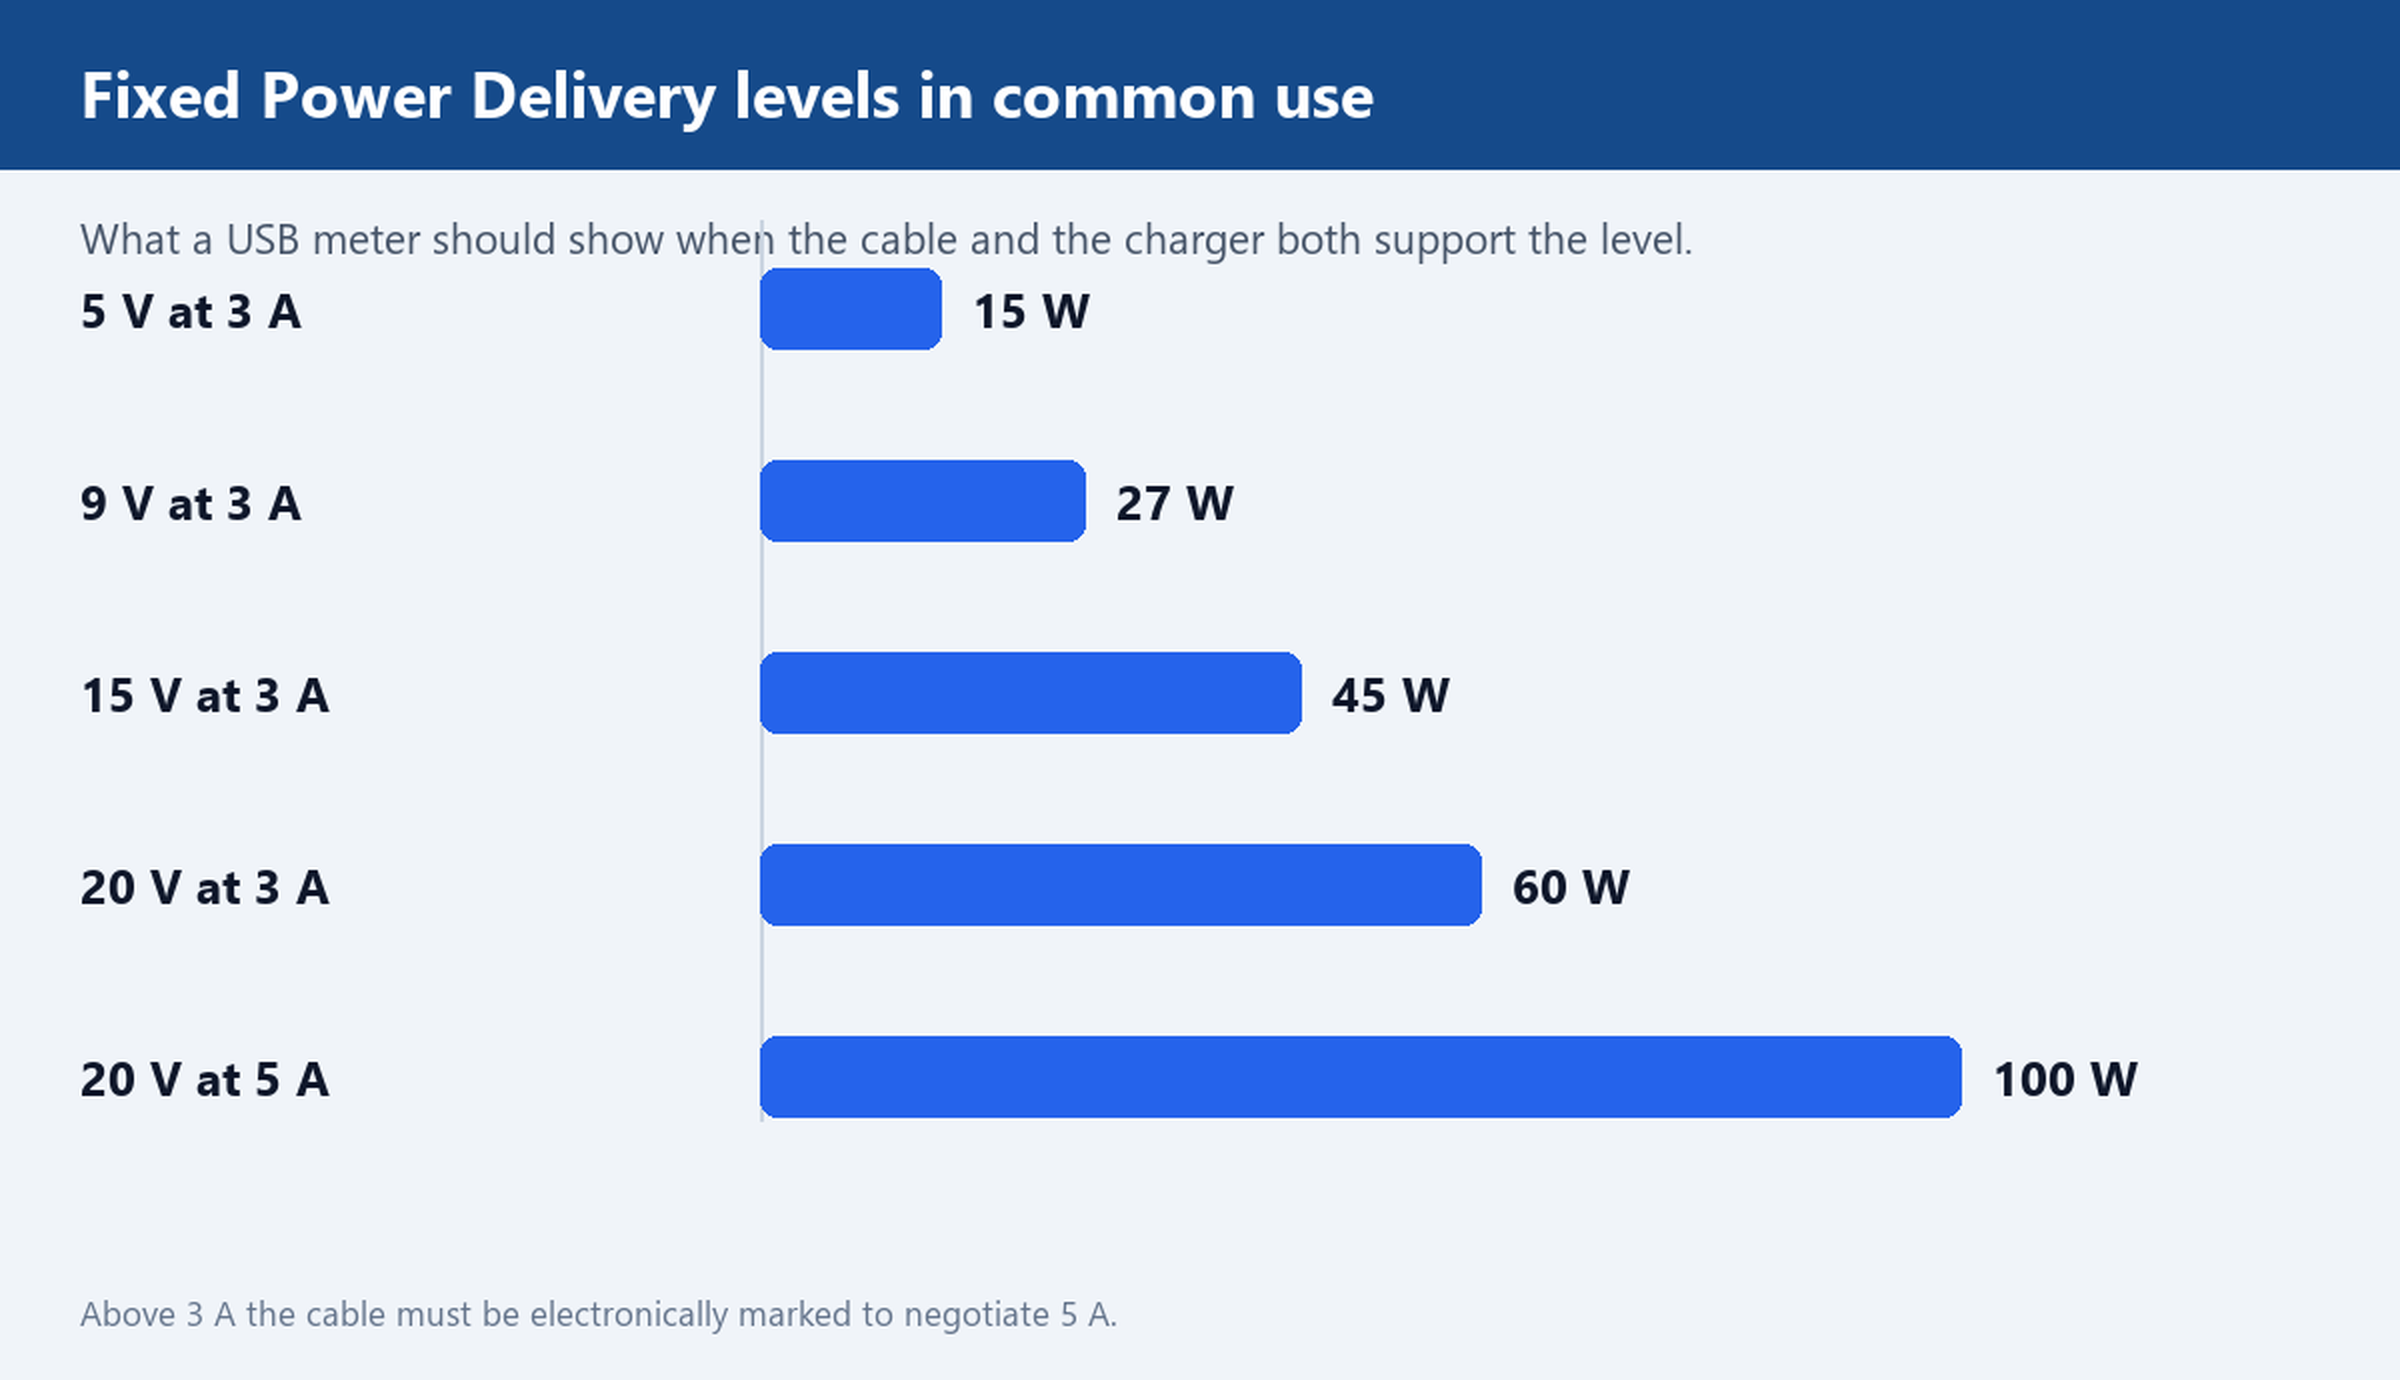
Bar chart of fixed Power Delivery levels: 15 W at 5 V 3 A, 27 W at 9 V, 45 W at 15 V, 60 W at 20 V and 100 W at 20 V 5 A
What a USB meter shows when cable and charger both support the level.

Signs a cable is failing mid-transfer

A healthy cable fails in patterns, and the pattern usually names the wire. These five symptoms cover most of the cases that reach a support desk:

  • Works in one orientation only. On a Type-C cable, flipping the plug should change nothing. If one side works, a data pair or a configuration channel line is broken.
  • Charges but never syncs. A charge-only build, or a data pair that has failed open. Both look identical from the outside.
  • Speed drops after a few minutes. Rising resistance at a damaged contact heats the connector, and the link falls back or drops.
  • Disconnects when the cable is moved. A conductor broken inside the jacket near the moulded end.
  • Slow-charge warnings. The device is reading a configuration channel or e-marker value it does not accept.

Check 1: pin-by-pin continuity with a multimeter

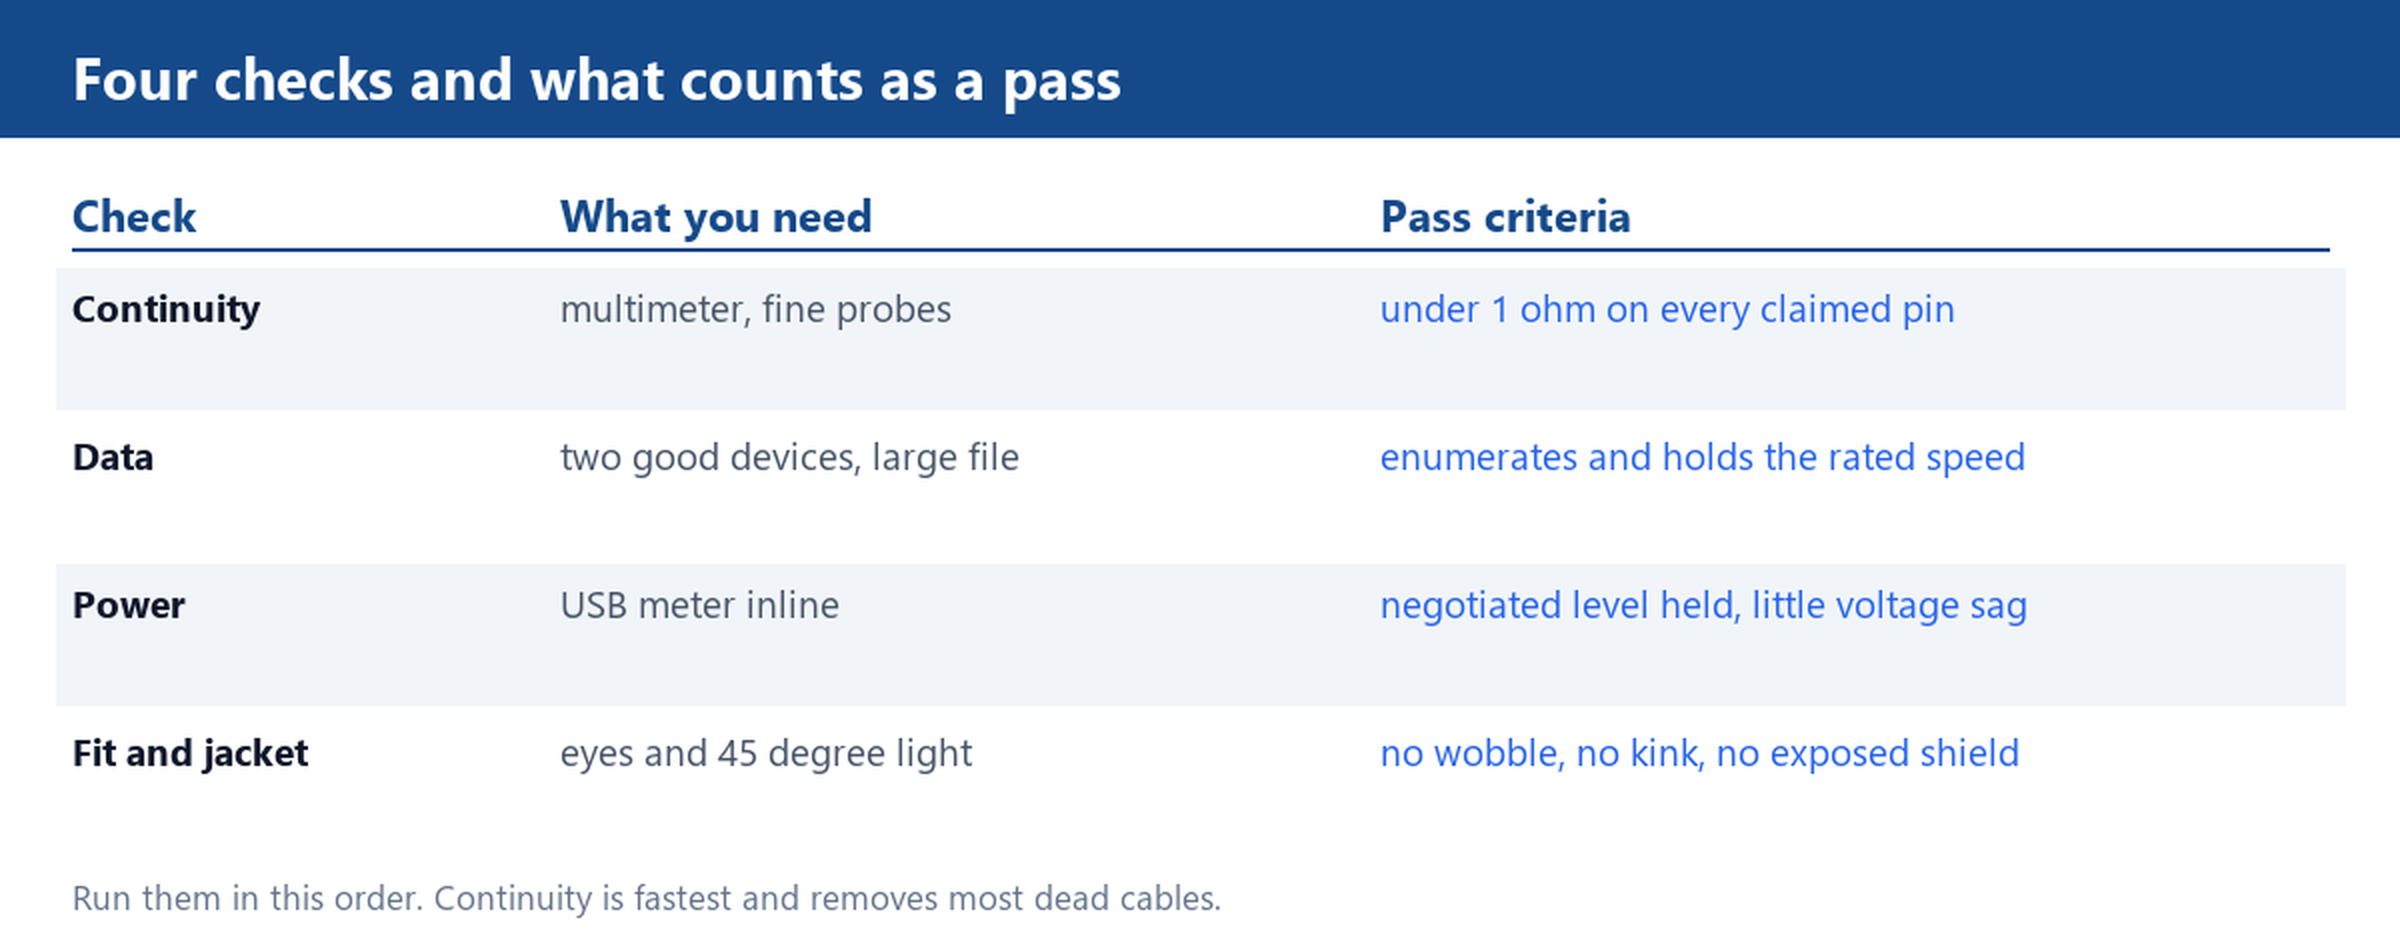
Unplug everything. Set the meter to continuity or low resistance and probe pin to pin at the two plugs, using fine probes so you are not shorting adjacent contacts.

For a USB-A to Type-C assembly, test VBUS, GND, D+, D-, CC1, CC2 and the shell. For a Type-C to Type-C assembly, test both CC pins and confirm the two orientations give the same result — that check alone catches the most common Type-C defect. For a SuperSpeed assembly, add the TX and RX pairs, because those can be open while the USB 2.0 pairs still work.

Pass criteria are simple. Every pin the cable claims should read under one ohm end to end. A pin that reads open, or drifts while the cable is flexed, has failed. Continuity between VBUS and GND means a short: stop testing and discard the cable, because the next device you plug in pays for it.

Table of four USB cable checks with the tool each needs and the pass rule: continuity, data transfer, power delivery and connector fit
Run them in this order. Continuity removes most dead cables.

Check 2: prove it is a data cable, not a charge-only build

Two known-good devices and one large file settle this. Connect them through the cable under test, transfer a file big enough to take more than a few seconds, and watch the reported link speed. A cable that carries power and nothing else will not enumerate storage at all.

If it does enumerate, compare the negotiated speed to what the cable is supposed to support. USB 2.0 tops out at 480 Mbps, USB 3.0 at 5 Gbps and USB 3.1 at 10 Gbps, and the link always runs at the lowest rate of the three participants: cable, host and device. A SuperSpeed cable on a USB 2.0 port will show 480 Mbps and is not faulty. A SuperSpeed cable on a SuperSpeed port that still shows 480 Mbps has an open pair, and the continuity check will usually name it.

Charge-only cables exist on purpose: many USB-A to Type-C assemblies ship with only power and ground. If the order needed data, that is a specification failure rather than a defect.

Check 3: measure the power path with a USB meter

Power faults are invisible to a continuity test because the wire is intact, just too thin. A USB meter inline between charger and device shows the negotiated voltage and the current actually flowing, and the difference between the two ends of the cable shows the loss.

Read the result against the delivery level the cable claims. The fixed Power Delivery levels in common use are 15 W at 5 V and 3 A, 27 W at 9 V and 3 A, 45 W at 15 V and 3 A, 60 W at 20 V and 3 A, and 100 W at 20 V and 5 A. Anything above 3 A requires an electronically marked cable, so a 5 A charger that only negotiates 60 W is telling you the cable did not identify itself. Voltage sag is the other signal: a cable dropping several hundred millivolts at 3 A is losing power in the copper.

Check 4: connector fit, port wear and jacket damage

Look before you measure, because some faults are visible. Inspect the plug under bright light at an angle:

  • Play. A plug that rocks in the port has worn retention features on one side, and the contacts wear faster than they should.
  • Debris. Compacted lint in a Type-C or Lightning port prevents full insertion and mimics a dead cable. Clean the port before blaming the cable.
  • Moulded ends. Cracks, whitening or a visible gap at the boot mean the strain relief has failed.
  • Jacket. Exposed shield, a permanent kink, or discolouration near the plug are end-of-life signs.

Then flex the cable gently at both ends while watching a transfer or a charge reading. A reading that flickers under flex confirms an internal break.

When to replace the cable instead of troubleshooting the device

Replace rather than investigate further when any of these is true: continuity fails on a pin the cable claims, VBUS and GND read as a short, the plug will not hold without wobble, the jacket shows a kink or a discoloured end, or speed and power both fall short of the rating on known-good hardware. Each is a cable fault, not an intermittent mystery.

For incoming batches, turn the same four checks into a bench routine. Keep one reference cable that is known good and never leaves the bench. Pull a sample from each carton, run continuity first because it is fastest, then a data transfer, then a meter reading under load, then a visual pass. Log the SKU, the carton and the result for every failure, and quarantine them instead of returning them to stock. A log with a carton number in it is what turns a complaint into a supplier conversation.

The cheapest way to avoid this routine is to test before the order: sample the USB cable you intend to buy and run the same four checks against your own devices. Our USB Type-C range includes assemblies such as the USB-C to USB-C 60 W cable built to be checked this way, and the USB 2.0 category covers the charge-and-sync builds. Tell us the devices and the current you need and we will point you at the right construction.

Read more...

Custom Audio Video Cable OEM: The Specs to Lock Before Ordering

Most custom cable quotes come back late because the request was incomplete, not because the factory is slow. A drawing that leaves out pinout, gauge, jacket, marking or packaging forces a round of questions, then a re-quote, and often a sample that fails on a detail nobody wrote down. The six fields below decide whether the first quote is usable.

This page is for the person building the RFQ on a custom audio video cable OEM program: what to lock, in what order, and what has to appear on the drawing so a factory can answer in one pass.

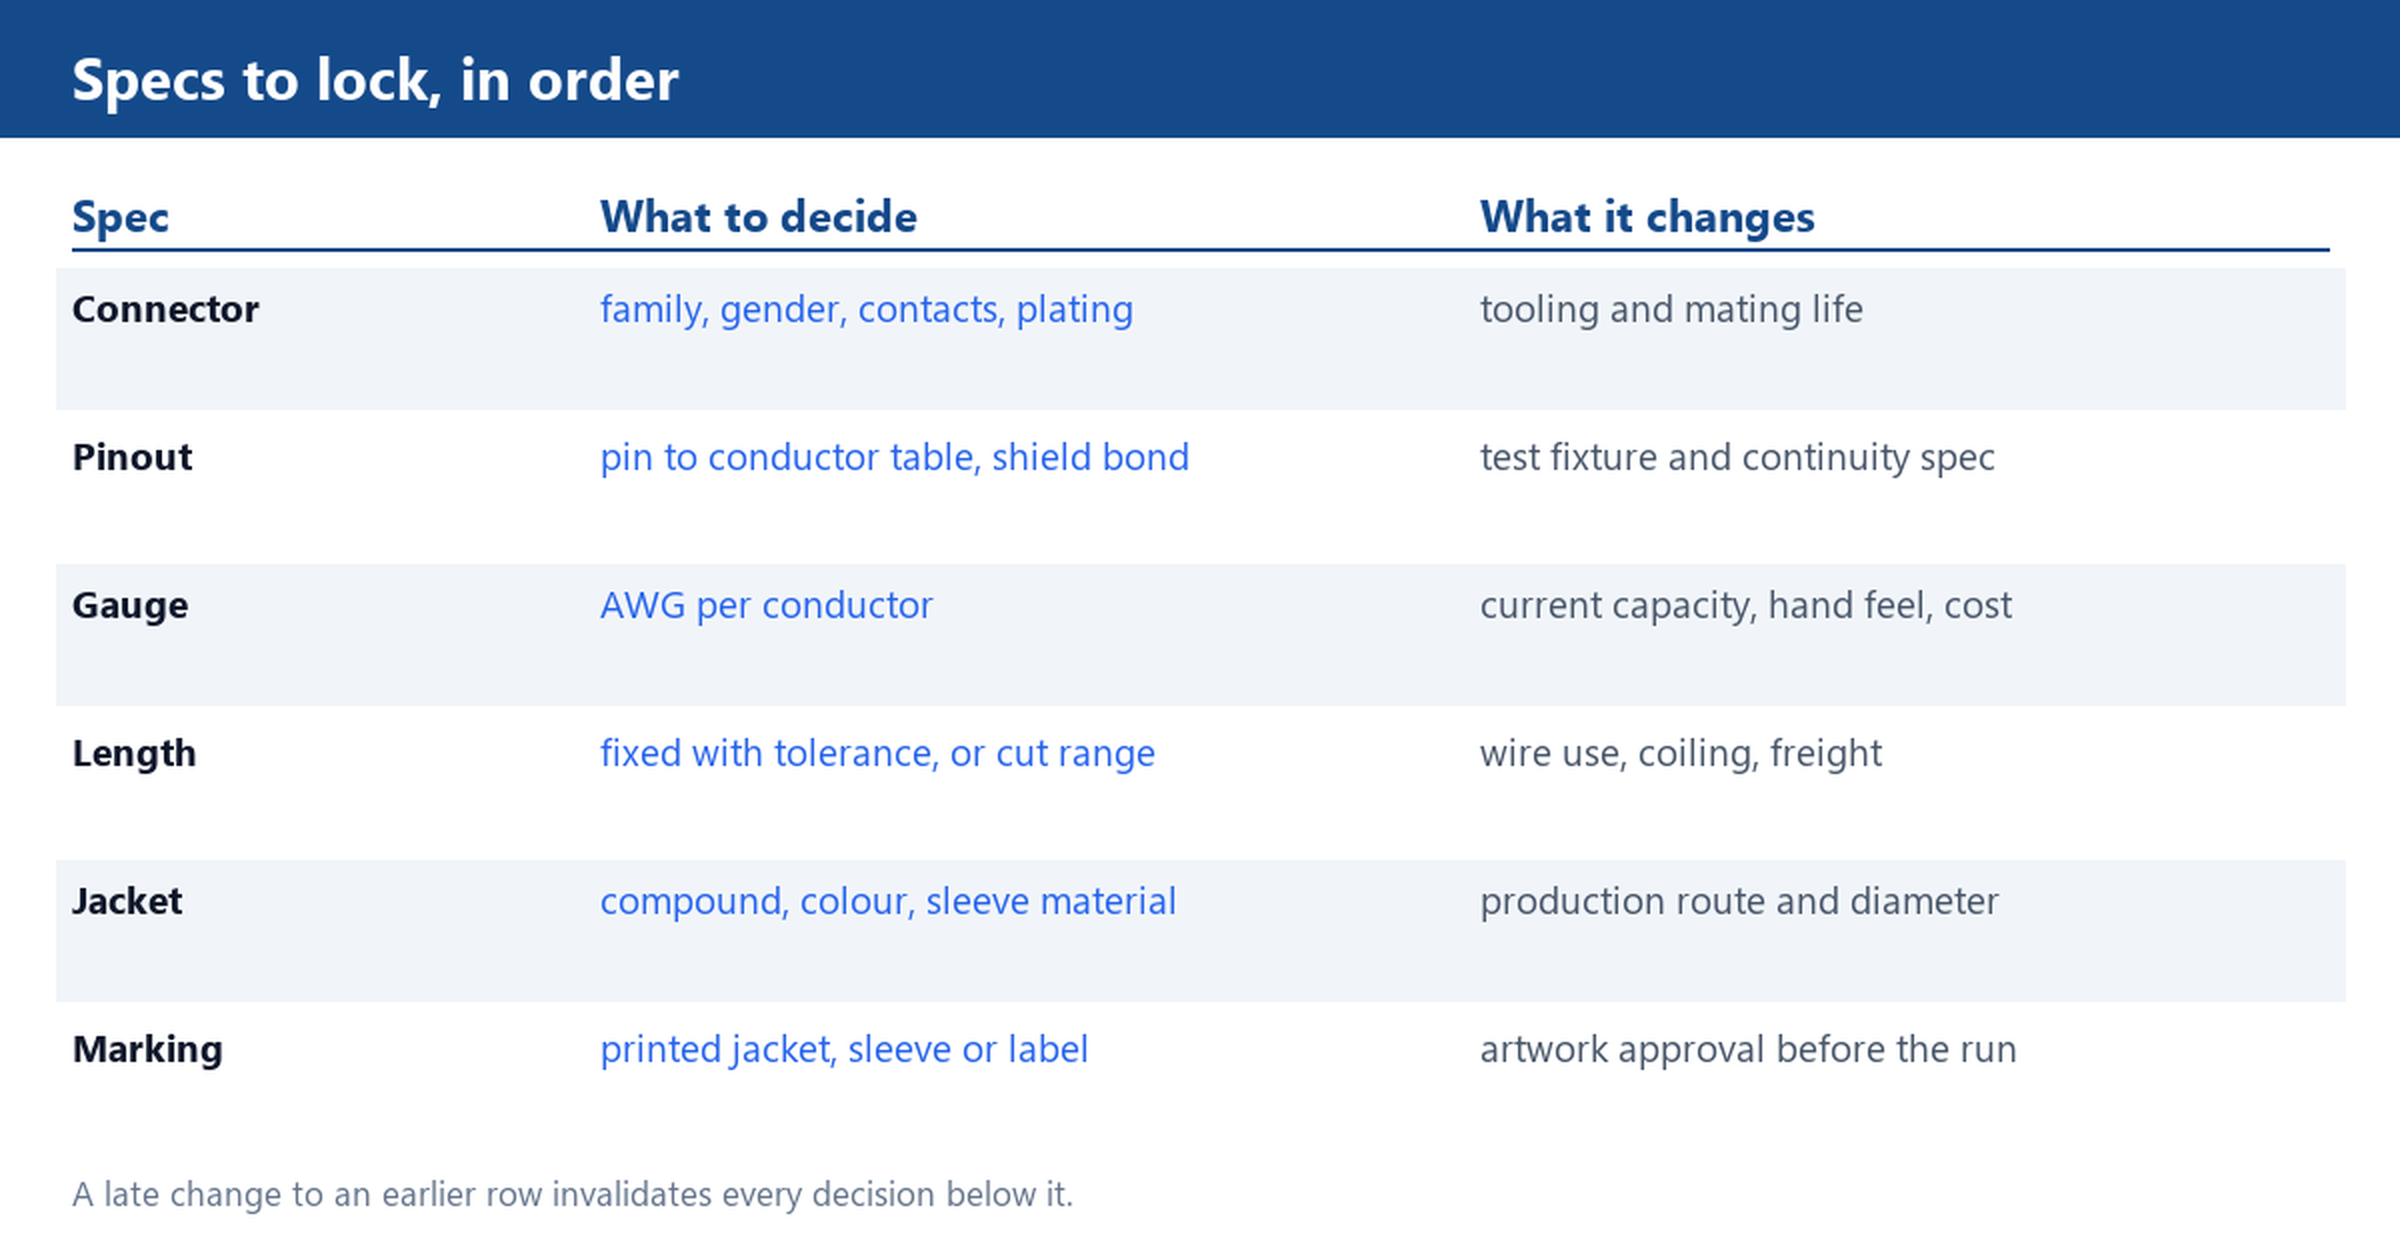
Table of six specs to lock before quoting a custom audio video cable, from connector and pinout through gauge, length, jacket and marking
Lock the rows top down. A change to an earlier row resets the rest.

The specs to lock before you ask for a quote

Six fields account for most of the cost difference between two otherwise similar assemblies, and they constrain each other in a fixed order.

Connector type and plating fix the tooling and the mating life. Pinout fixes the test fixture. Gauge fixes current capacity and hand feel. Length fixes wire consumption and packing. Jacket fixes the production route. Marking and packaging fix the approval cycle, which is usually the long pole — artwork sign-off, not the cable, is what holds a run.

The order matters: a late change to an earlier field invalidates every decision after it, and a jacket change after the sample means a new production route.

Connector and pinout: what belongs on the drawing

Name the connector family, the gender, the contact count and the plating. For audio and video assemblies that usually means an XLR 3-pin plug, a 6.35 mm TS or TRS plug, an RCA, a Speakon, or a 3.5 mm TRRS jack. Plating deserves more attention than it gets: nickel is the sensible default, and gold is for repeated mating against gold contacts.

Pinout belongs on the drawing as a table, never as a sentence. For a balanced XLR assembly, state pin 1 to shield or drain, pin 2 to tip or positive, pin 3 to ring or negative, and say whether the shell bonds to the shield. For a TRS to dual RCA splitter, state which conductor lands on which RCA centre pin. If the part is an adapter, add the direction: male to female, or female to male.

This is the most common cause of a wasted sample. Two factories can build the same connector list and produce two electrically different parts, and neither is wrong until the drawing says which one it wanted.

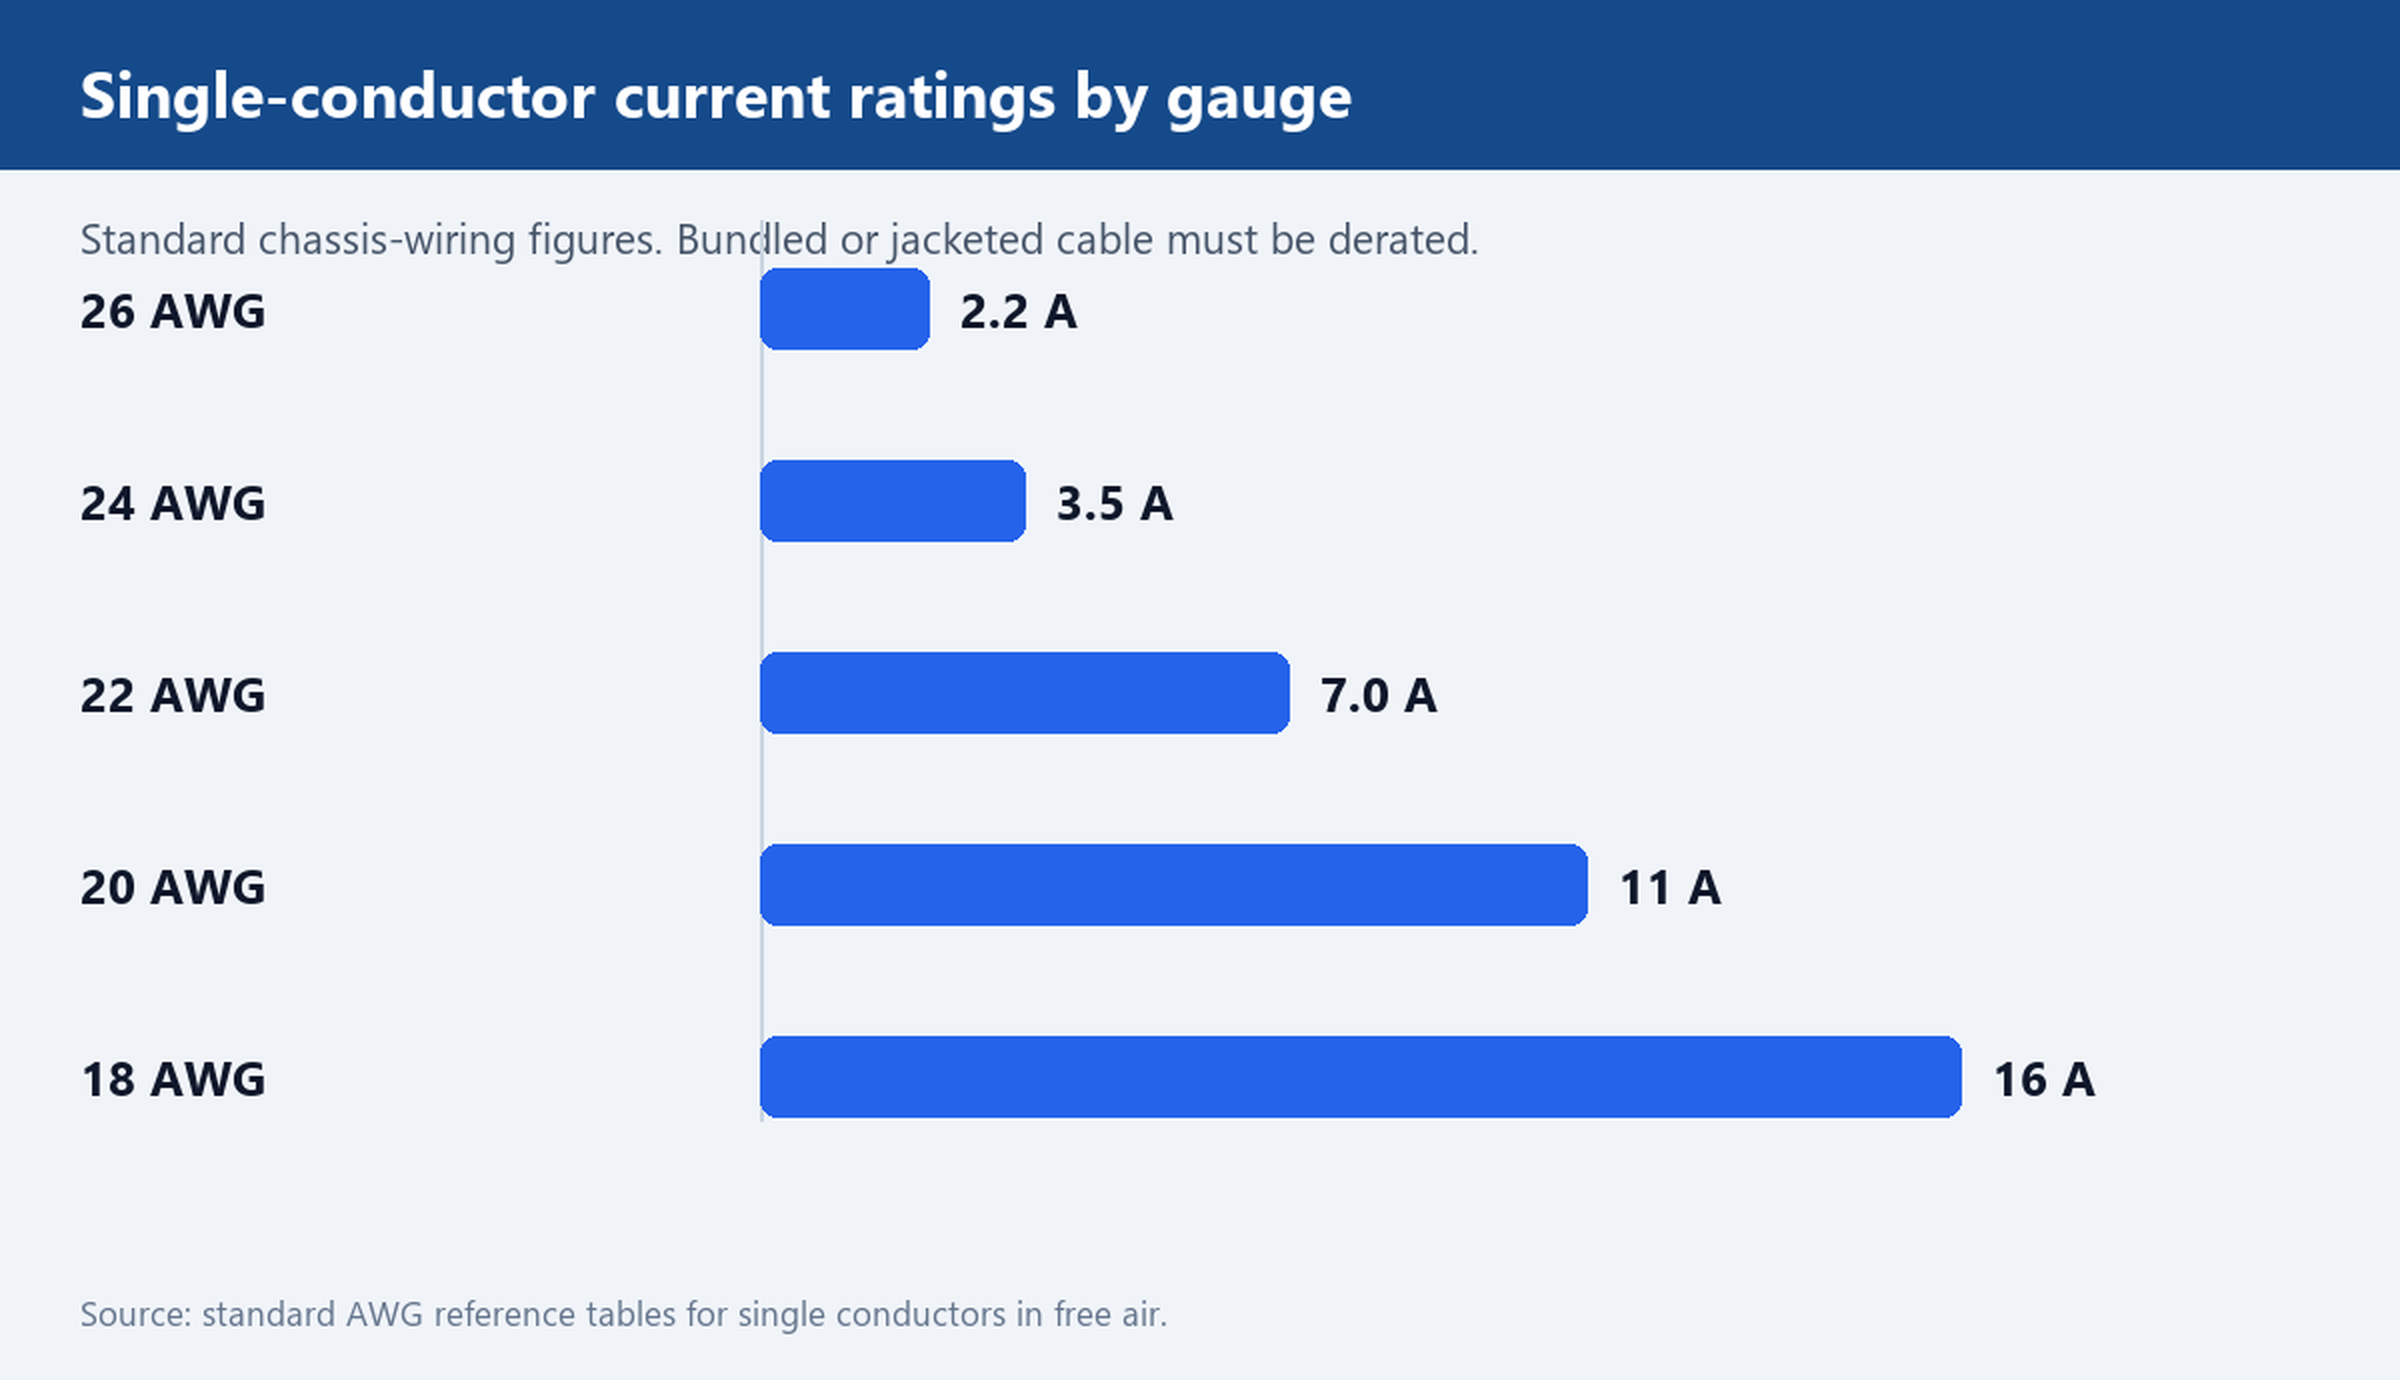
Bar chart of single-conductor current ratings by gauge: 26 AWG 2.2 A, 24 AWG 3.5 A, 22 AWG 7 A, 20 AWG 11 A and 18 AWG 16 A
Single-conductor figures. A bundled run carries less.

Length, gauge and shielding: how each one moves the cost

Gauge sets current capacity and hand feel at once. For a speaker run, 12 AWG to 16 AWG covers most stage work; for a line-level patch, 20 AWG to 24 AWG is normal. The chart above gives standard single-conductor chassis-wiring figures, and any bundled or jacketed run has to be derated from them because heat cannot escape the same way.

Length is not just more wire. It changes coiling, packing, freight weight and sometimes the strain relief. Specify fixed lengths with a tolerance, or a cut range, and state whether the length is measured over the moulded ends or pin to pin.

Shielding is where thin quotes hide. Foil plus a drain wire is the economical choice for line-level runs that never move. A spiral copper shield suits microphone cable that will be coiled thousands of times. A braided copper shield gives the highest coverage and adds cost and stiffness. Put the coverage percentage on the drawing, because a shield with no stated coverage cannot be checked at incoming inspection.

Strain relief, jacket and overmould: the parts buyers leave off

Three details decide whether the assembly survives its first month, and all three are usually missing from a first RFQ.

Strain relief. State the moulded boot length, the flex direction if the part is right-angled, and whether the assembly must pass a pull test. A right-angle plug with a long boot does not fit the same panel cutout as a short one.

Jacket. Name the compound and the colour, and say whether printing goes on the jacket or on a sleeve. For a braided construction, add the sleeve material, because nylon and polyester behave differently under abrasion and under flame.

Overmould. Specify hardness and finish. A soft mould grips and hides a poor fit; a hard mould holds shape but can crack at the boot if the compound is wrong for the temperature.

Labeling, packaging and kitting for retail-ready orders

If the cable goes on a shelf, the packaging carries as much of the order as the cable does:

  • Marking. Part number, length and rating printed on the jacket, on a heat-shrink band, or on a wrap label.
  • Unit pack. Poly bag, zip bag with a header card, or a printed box. Bag dimensions change the carton count and the freight cost.
  • Multipacks. A two-pack or six-pack needs its own artwork, its own bag and its own carton count.
  • Artwork files. Supply vector files with fonts converted, plus a dieline for any printed carton. Raster artwork gets redrawn by someone, and that is where brand errors enter.

None of this changes the cable. All of it changes the schedule.

What the factory needs to quote in one round

A complete RFQ for a custom audio video cable assembly carries seven things: connector list with plating, pinout table, gauge per conductor, length with tolerance and measurement basis, jacket compound and colour, shield type with coverage, and marking plus packaging artwork. Add the quantity by configuration and the destination, and the quote needs no assumptions.

Two notes on sending it. A marked-up photo is acceptable as a starting point but must be replaced by a drawing before tooling. And say which fields are fixed: a factory that knows gauge is negotiable will suggest a cheaper gauge.

When a second sample round happens, the cause is nearly always one of four things: an ambiguous pinout, an unstated length measurement basis, artwork that arrived as a raster file, or a jacket change requested after the first sample. Each is preventable at the RFQ stage.

Send the drawing or spec sheet as you have it, even incomplete, and we will mark what is missing and confirm feasibility against the build you intend to run. The audio and video cable category shows the constructions we run most often, including the 12 AWG Speakon speaker assembly. The customize cable page covers the options, factory covers the process, and how to order lists what a first RFQ should carry.

Read more...

Braided vs PVC Cable: Choosing the Right Jacket for Your Order

Two cables built on the same copper can feel nothing alike in the hand, and the jacket is almost always why. Buyers weighing braided against PVC want one answer: which construction survives the way this cable actually gets used. Braid buys abrasion resistance, grip and a softer drape. PVC buys lower unit cost, a smaller outer diameter and predictable tooling. Braid does not buy heat resistance, better shielding or longer life on its own, and plenty of change requests arrive with that assumption attached.

This guide covers what each jacket is, where each one really wins, and how the braided vs PVC cable decision moves tooling, artwork approval and repeat orders.

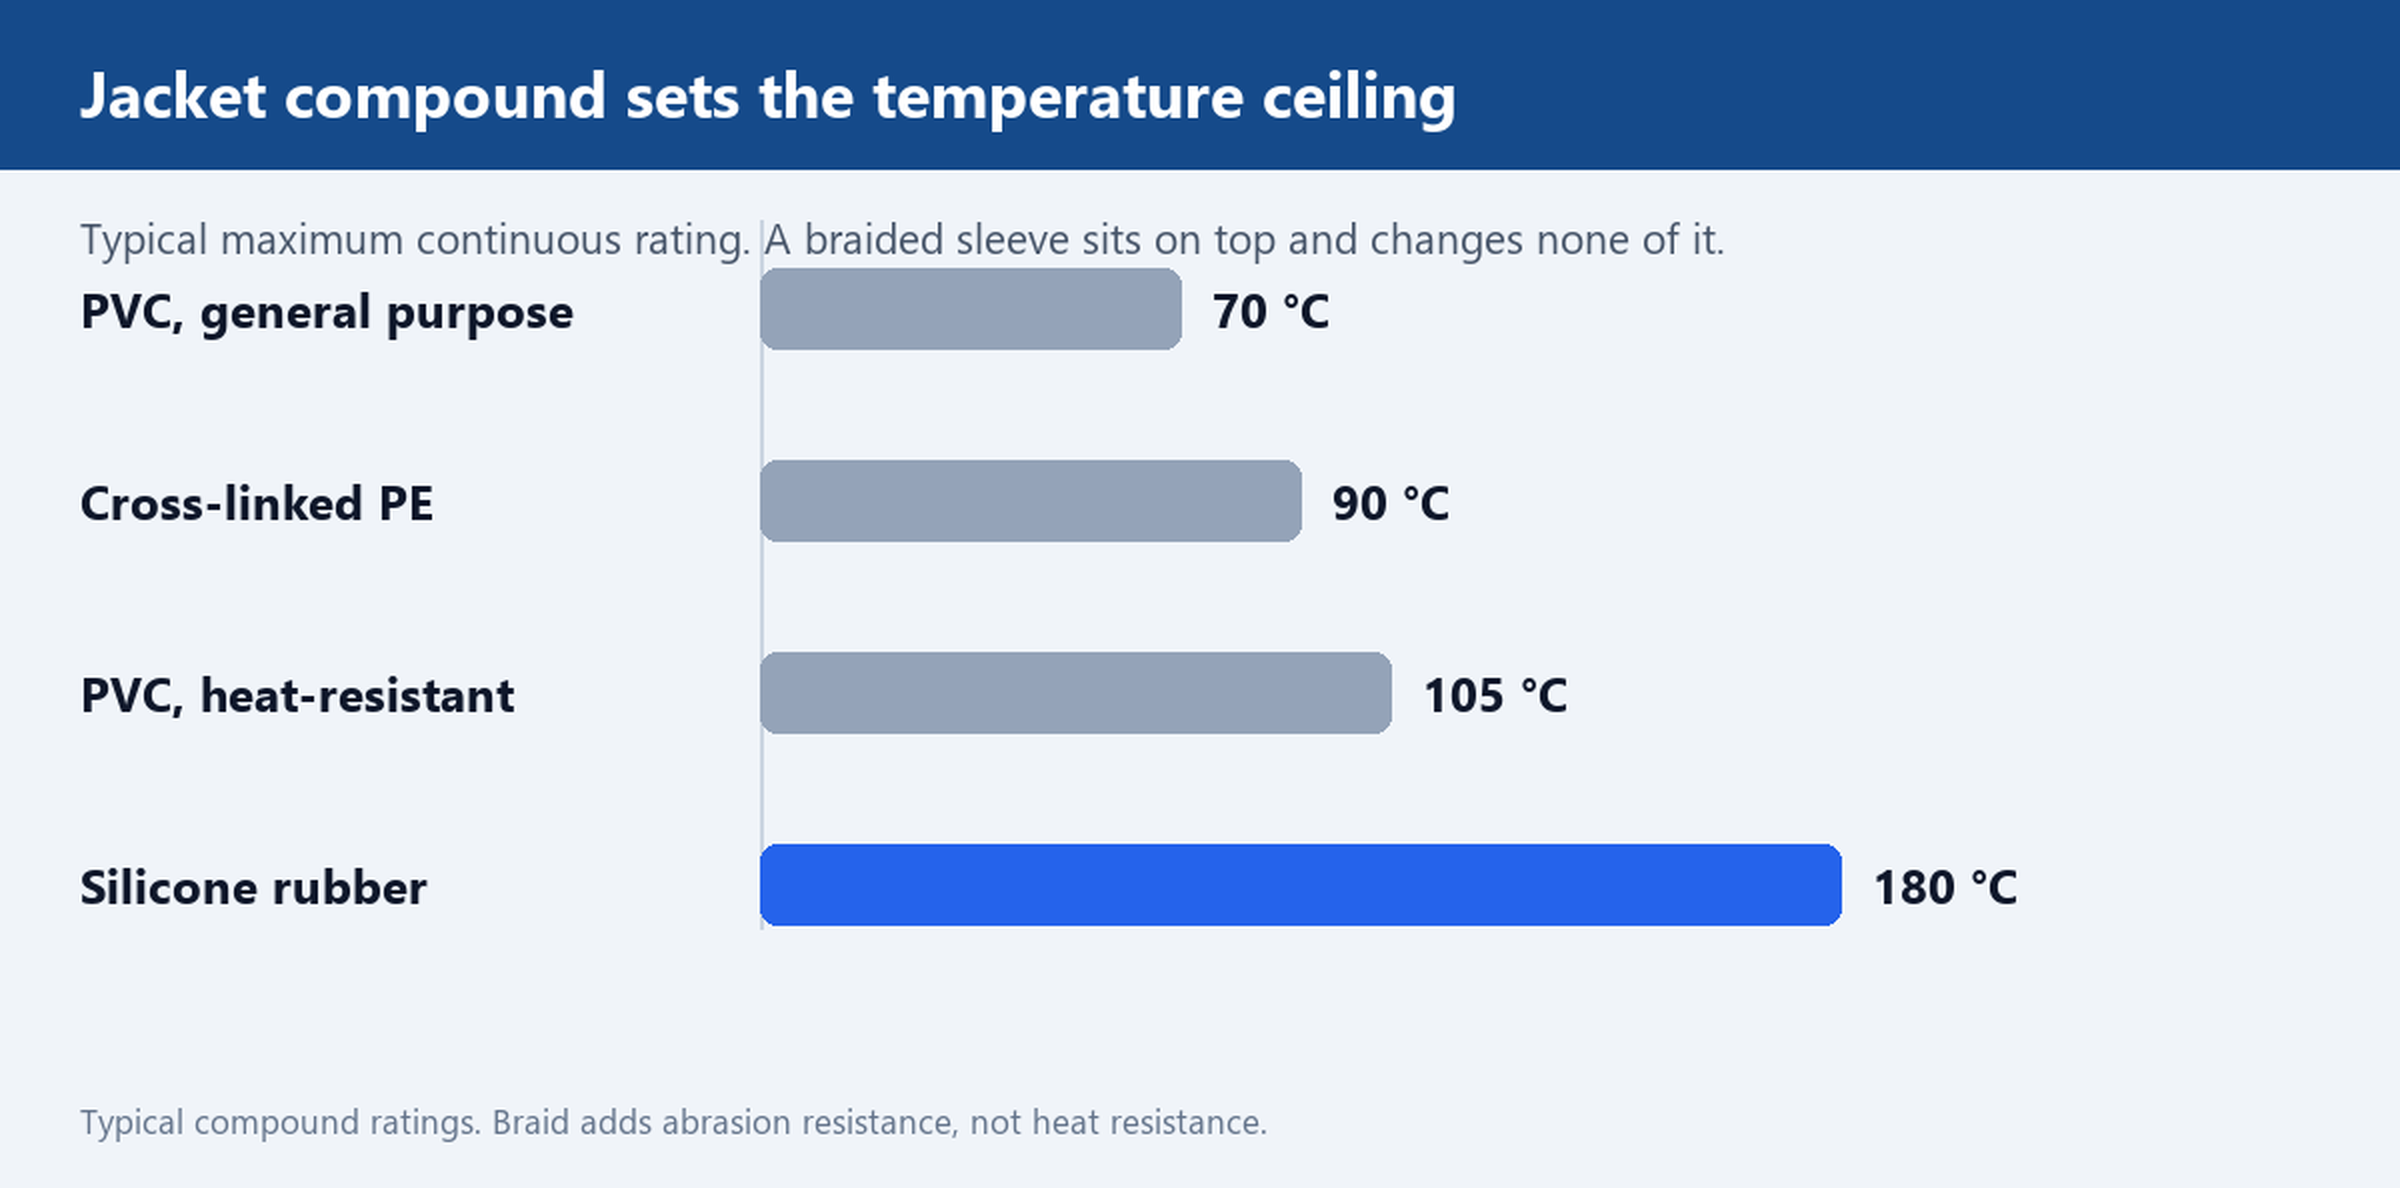
Bar chart of typical temperature ratings by jacket compound: PVC 70, cross-linked PE 90, heat-resistant PVC 105 and silicone 180 degrees Celsius
The compound sets the limit, not the weave.

What each jacket is actually made of

A PVC cable is a conductor bundle with extruded polyvinyl chloride over it, produced in a single pass at a fixed outer diameter. The compound is formulated for flexibility, flame behaviour and surface finish, and the extrusion die sets the diameter everything downstream depends on.

A braided cable adds a woven textile sleeve over that same core, usually nylon or polyester, often over a second thin jacket. The braid is a sleeve. It is not insulation and it is not the flame barrier. Ask which layer carries the temperature or flame rating and the answer points to the compound underneath.

That fact settles most arguments in this category. A braided assembly is mechanically different from a PVC one and electrically the same, unless the buyer also changes stranding, shield coverage or gauge.

Where braided construction earns its cost

Braid solves mechanical problems well in four situations:

  • Sliding abrasion. Cables dragged across stage floors or rolled under pedalboards wear on the outer surface first. A tight weave spreads that contact across many filaments instead of one smooth wall.
  • Point loads. A truss clamp pinches a cable in one spot. Braid spreads the load around the circumference, which keeps the jacket from taking a permanent set.
  • Grip and drape. Textile does not go slick when hands are damp and hangs with fewer kinks than a glossy extrusion.
  • Surface appearance. A matte weave hides scuffs that show immediately on gloss PVC, which matters for rental fleets and product photos.

For a braided microphone cable, the construction and gauge make the difference checkable rather than a finish claim. The balanced braided XLR assembly is a useful reference build, and the microphone and XLR cable category covers the range.

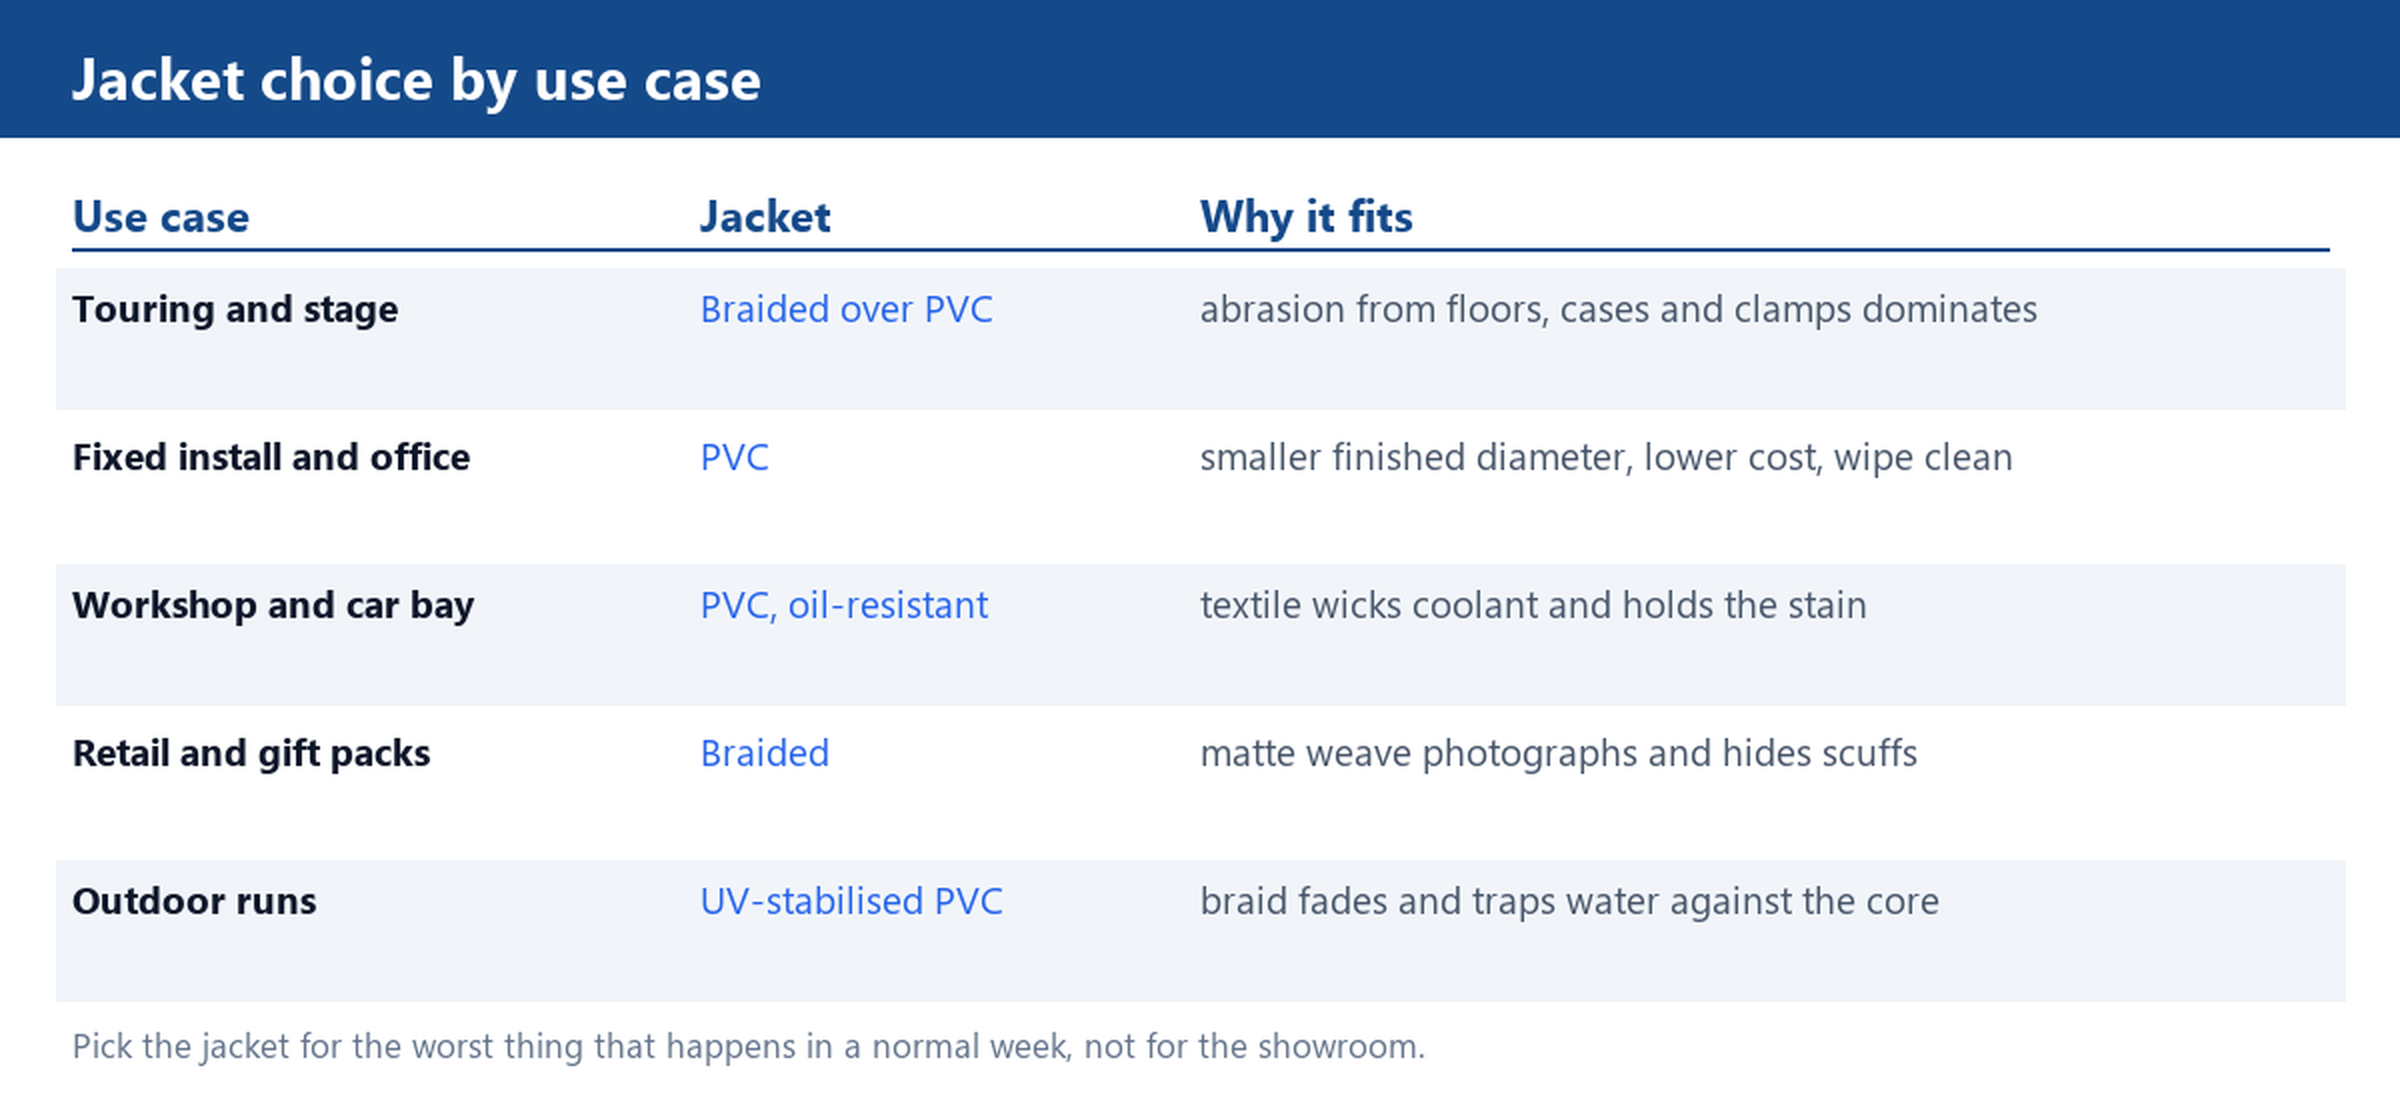
Table mapping five use cases to a jacket: touring and retail to braided, fixed install and workshop to PVC, outdoor runs to UV-stabilised PVC
Pick for the worst thing that happens in a normal week.

Where PVC is the practical choice

PVC wins on what appears in a purchase order rather than a product photo:

  • Unit cost. One extrusion pass, against an extrusion plus a braiding step, plus yarn, plus end finishing.
  • Outer diameter. At the same conductor and shield, PVC gives the smaller finished diameter, which decides whether the cable fits a backshell, a grommet or a conduit.
  • Cleanability. A shop rag with a mild solvent takes grease off PVC. Textile absorbs it and holds the stain.
  • Marking. Length marks and part numbers print directly on PVC. On braid they need a sleeve or a printed band, which is a separate artwork approval.

For fixed installs, patch panels and OEM builds where the cable is never handled, PVC is usually the sound answer. The PVC XLR range exists for exactly that reason.

What the jacket does not change

Four properties stay where they were, whatever the outer layer looks like:

  • Temperature ceiling. Set by the compound, not the weave. General-purpose PVC is commonly rated to 70 °C, heat-resistant grades to 105 °C, cross-linked polyethylene to 90 °C and silicone to 180 °C. Braid over a 70 °C core is still a 70 °C cable.
  • Shielding. Foil, spiral or braided copper shield decisions sit under the jacket and decide interference performance. A textile sleeve does nothing for shielding.
  • Conductor and gauge. Voltage drop, current capacity and flexibility all come from the copper and the stranding.
  • Connector plating. Contact life and mating cycles are a connector decision.

If a project needs a higher temperature rating, the fix is a different compound, not a braid. That is the most common mis-buy here and the easiest to prevent with a two-line spec.

Matching the jacket to the use case

Name the worst thing that will happen to the cable in a normal week — dragged over a floor, crushed in a bag, coiled wet, or never touched — then match it:

  • Touring and stage. Braided over PVC, because abrasion and handling dominate every other property.
  • Fixed install and office. PVC, because nothing touches it and diameter matters.
  • Workshop and automotive bay. PVC in an oil-resistant grade, because textile wicks coolant.
  • Retail and gift packaging. Braided, because the unboxing is part of the product.
  • Outdoor runs. Neither on its own. Specify a UV-stabilised compound and a path for water to drain.

How the choice changes tooling and repeat orders

Braid adds process steps: yarn sourcing, a braiding pass, and end finishing so the sleeve does not fray at the cut. Those steps lengthen the production cycle and add parameters to hold constant between lots. PVC adds none of that, but it locks in the extrusion die, so a diameter change on a repeat order means new tooling.

Either way, four items belong in writing before the first run: the compound and its rating, the finished outer diameter with a tolerance, a physical colour reference rather than a colour name, and the marking method — printed on the jacket, or on a sleeve. Agree those four and a repeat order becomes a part number. Leave them verbal and every lot becomes a negotiation.

Jacket samples of both constructions can ship with any quote. Send the drawing with the compound, the finished diameter and the marking method, and we will confirm feasibility. The customize cable page lists the options, and how to order lists the drawing fields we need.

Read more...

USB Cable Versions Compared: 2.0 vs 3.0 vs 3.1 for Buyers

Ask a supplier for a USB cable and you will get a dozen follow-up questions: which version, which connector, how long, what gauge. The version number is the one that matters most, because it decides whether the cable can move data fast enough for the device on the other end. This guide breaks down how USB cable versions differ in plain terms, and how to match each one to the application in front of you.

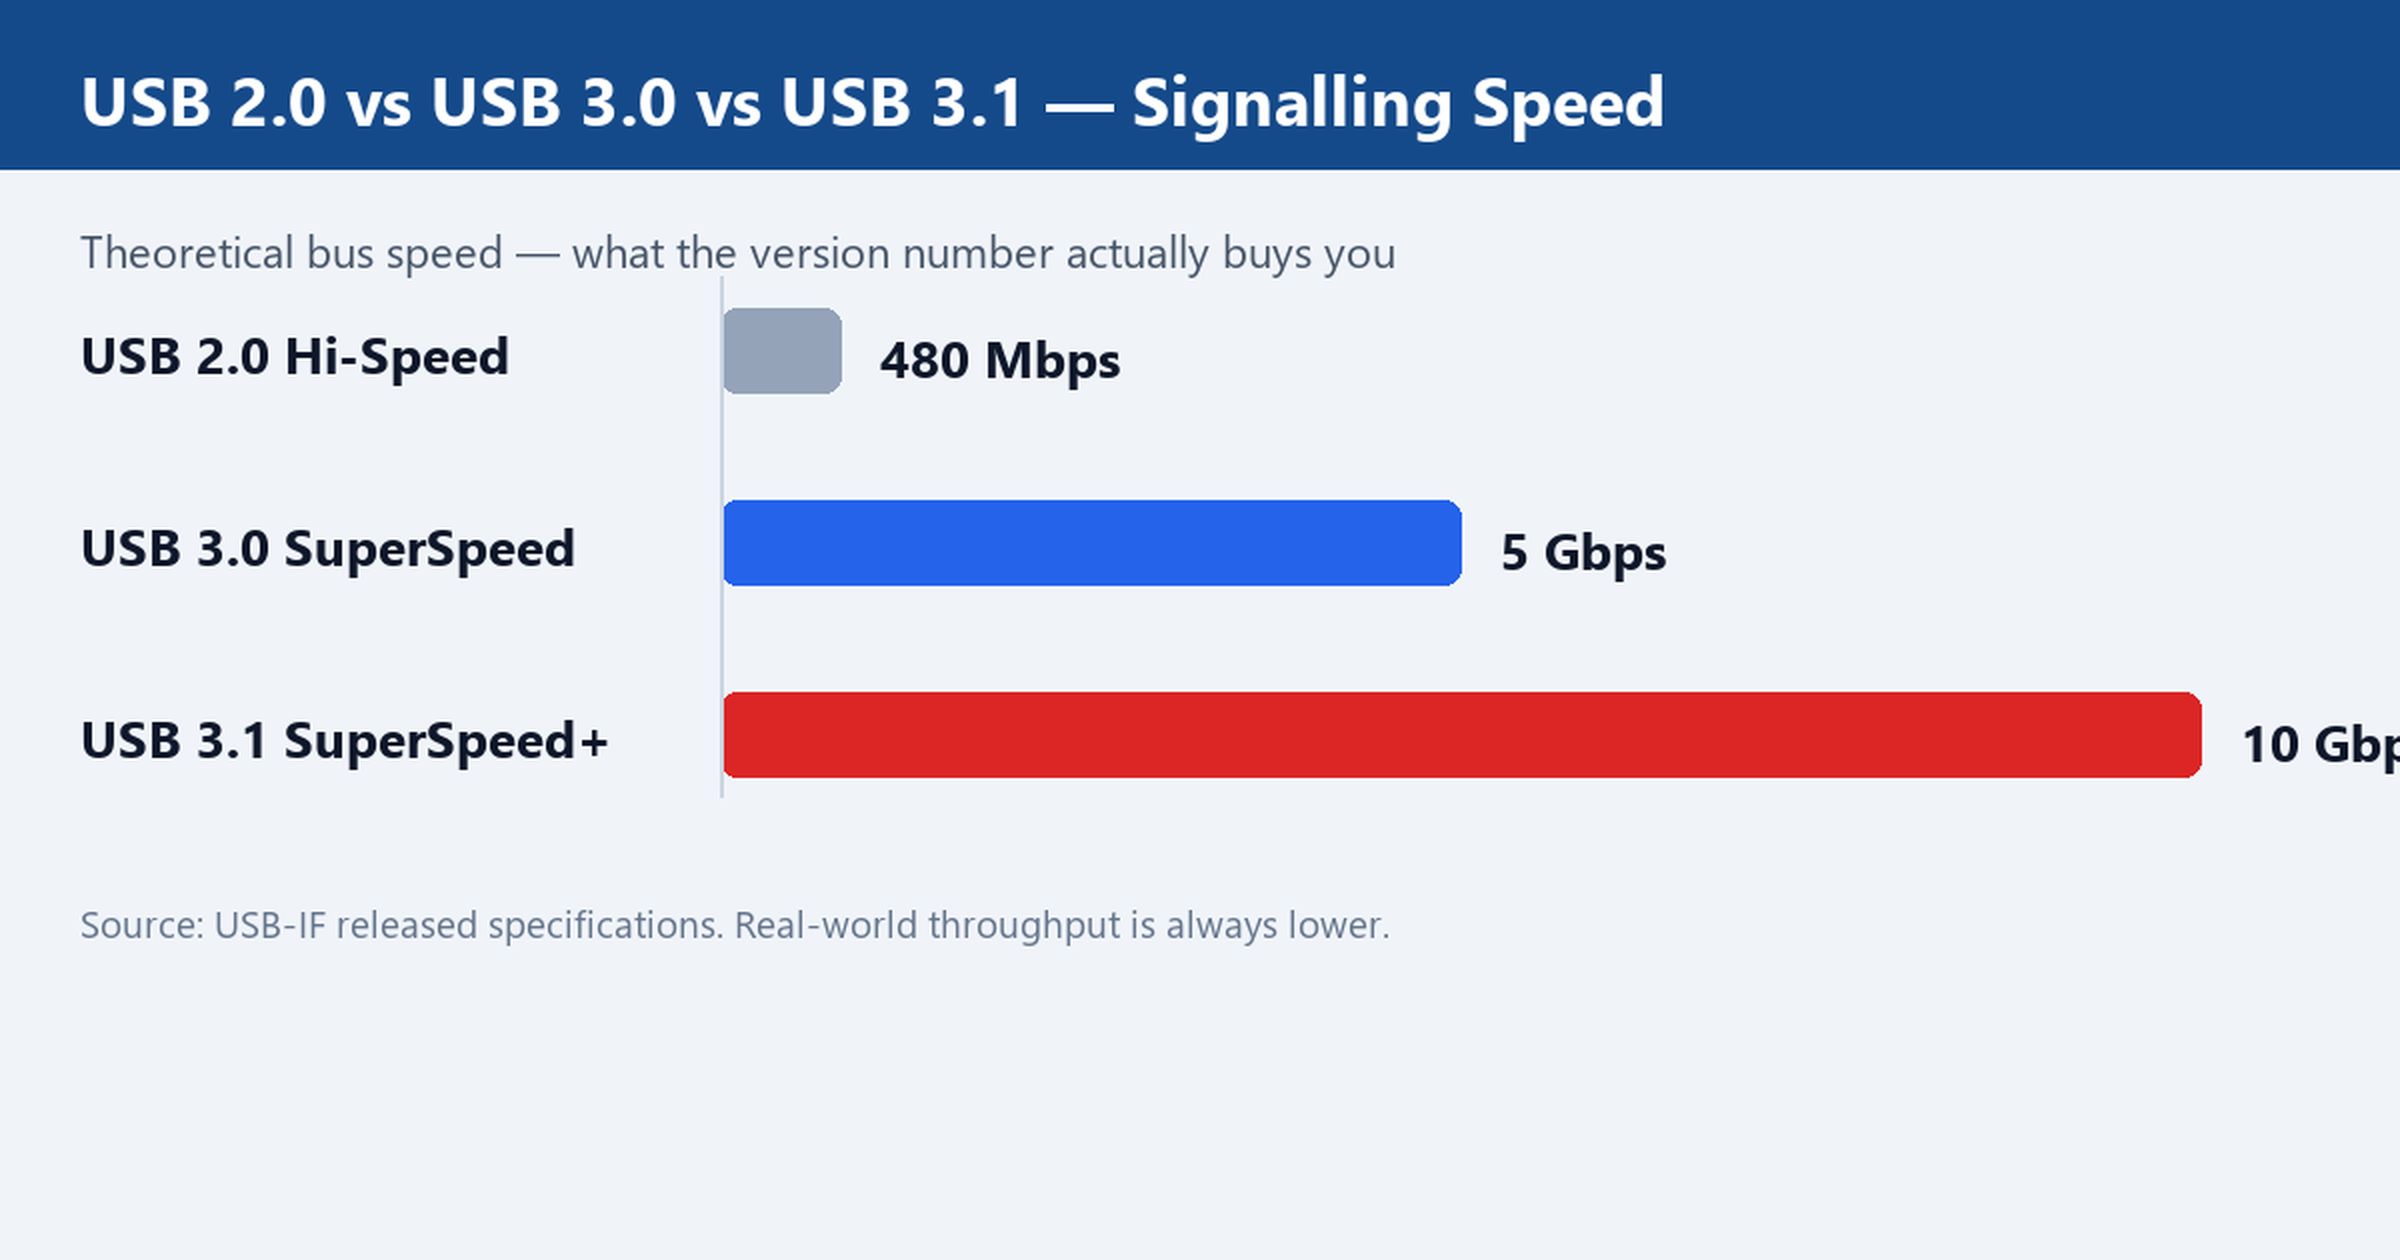
Bar chart comparing theoretical bus speeds of USB 2.0 at 480 Mbps, USB 3.0 at 5 Gbps and USB 3.1 at 10 Gbps
Theoretical signalling rates by USB version, per the released specifications.

What the version number actually means

USB versions are signalling standards, not connector shapes. A cable can carry a Type-C connector and still be a USB 2.0 cable inside, which is exactly why so many orders go wrong. The version tells you the maximum bus speed, the number of data pairs inside the jacket, and how the cable negotiates power.

USB 2.0 Hi-Speed runs at 480 Mbps over a single differential pair. USB 3.0 SuperSpeed adds two more pairs and lifts the ceiling to 5 Gbps. USB 3.1 keeps the same connector family but pushes signalling to 10 Gbps and tightens the rules around power negotiation. If you remember one rule, make it this: the version sets the ceiling, and everything else on the bus has to live under it.

USB 2.0 — still the right choice for charging and simple devices

Most USB cables sold worldwide are USB 2.0, and for good reason. Charging does not need bandwidth: the negotiation between a charger and a phone happens over a few control messages, and 480 Mbps handles that with room to spare. Keyboards, mice, card readers, firmware-update cables and point-of-sale peripherals all sit comfortably inside the USB 2.0 envelope.

For buyers, USB 2.0 is also the economical tier. Cables in this family are usually shorter, thinner and cheaper to tool, which makes them the default for promotional items and accessory bundles. If your application is charge-and-sync, a USB 2.0 cable from our catalogue will do the job without paying for bandwidth nobody uses.

USB 3.0 — when bus speed becomes the bottleneck

The moment storage or imaging enters the picture, USB 2.0 stops being enough. External hard drives and SSD enclosures saturate a 480 Mbps link in seconds. Printers, scanners and machine-vision cameras queue up image buffers faster than a USB 2.0 bus can drain them. USB 3.0 answers this with a 5 Gbps signalling rate, which clears those queues and leaves headroom for the next device generation.

USB 3.0 also introduced the familiar blue connector tab and the wider Micro-B plug, so you can often identify the version by eye. When sourcing, check that the jacket and the connector both match the spec you need: a USB 3.0 Micro-B cable with a 2.0 core will pass a visual check and fail on the bench. Our USB 3.0 cable range covers the printer, hard-drive and hub variants that B2B buyers ask for most.

USB 3.1 and Type-C — speed plus power negotiation

USB 3.1 is where the modern cable world lives. Signalling goes to 10 Gbps, and because the standard is written around Type-C, the same cable can carry data, display output and up to 100 W of power in both directions. That convergence is why docking stations, 4K capture dongles and laptop chargers have all standardised on Type-C hardware.

One caution for buyers: Type-C describes the connector, not the speed. A Type-C cable can be USB 2.0, 3.0 or 3.1 inside, and only the specification sheet tells you which. Look for the SuperSpeed or SuperSpeed+ marking, or ask the supplier to confirm the signalling rate in writing. Our USB 3.1 cable and USB Type-C cable lines are separated by signalling rate precisely so this confusion does not reach your warehouse.

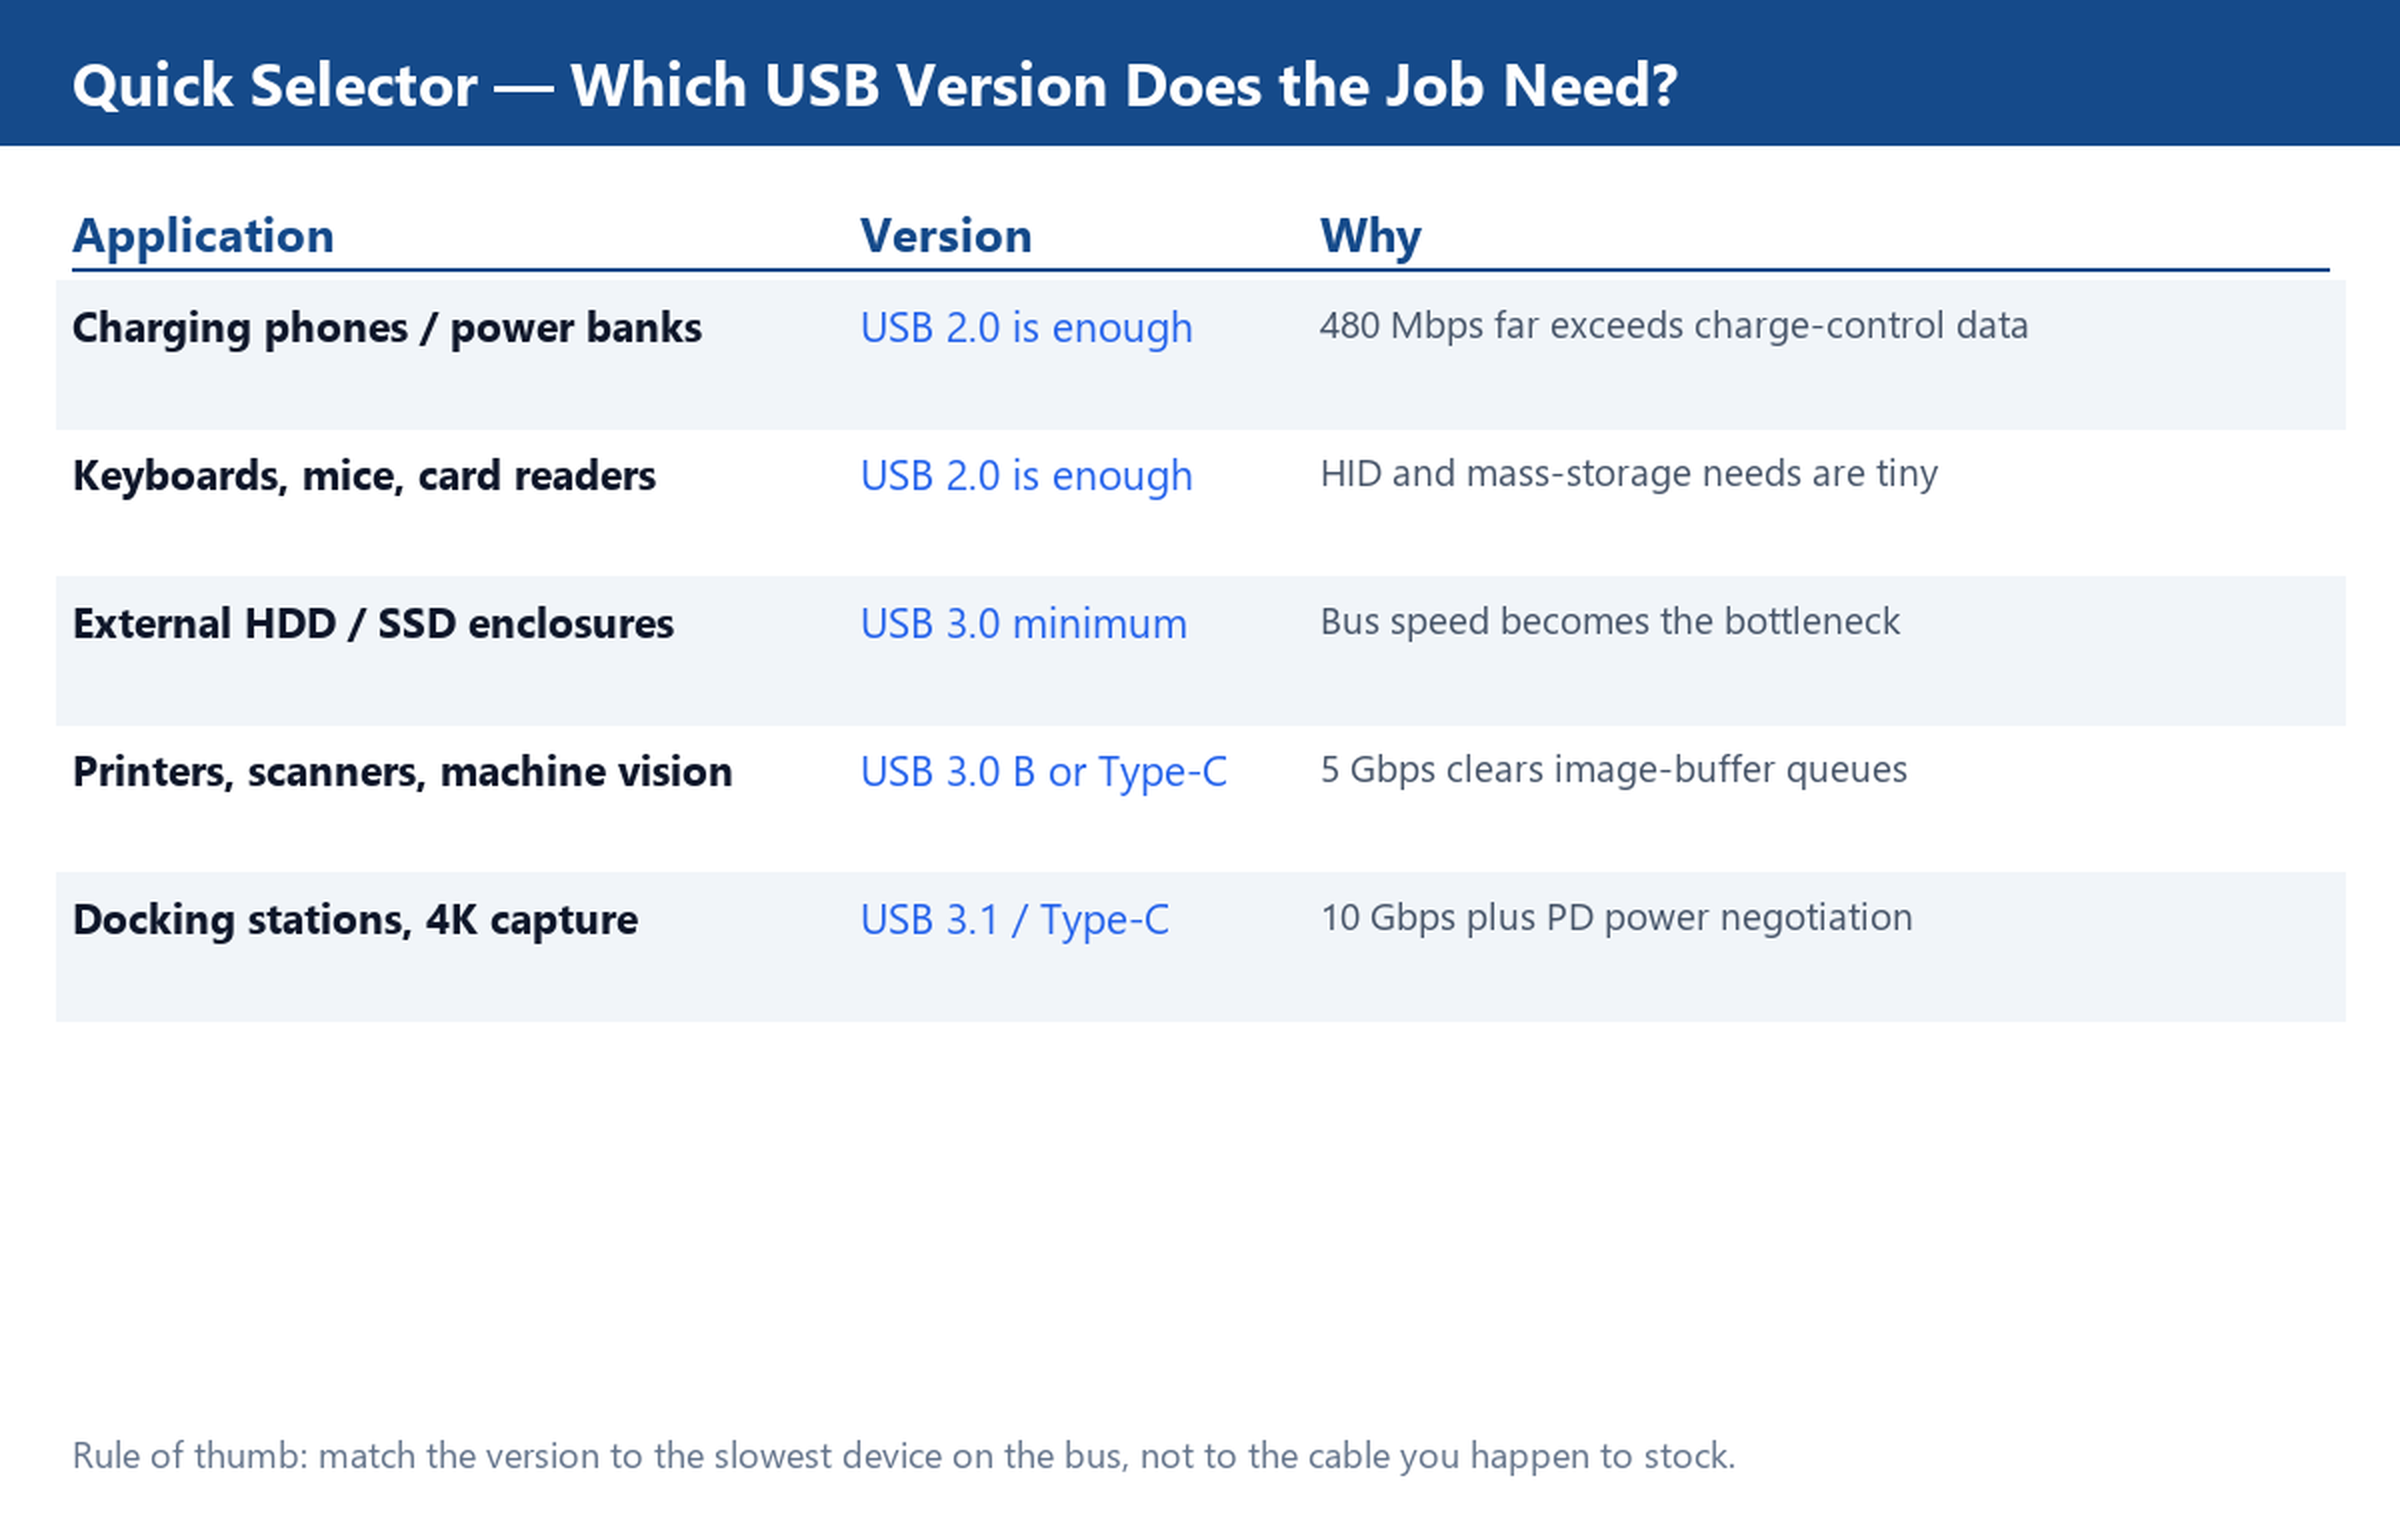
Selector table matching common applications such as charging, card readers, external drives and docking stations to the minimum USB version required
Match the version to the slowest device on the bus, not to the newest one.

Length, gauge and shielding: the specs buyers forget

Version is only half the specification. The other half is the physical build, and it decides whether the cable survives real use.

Length is the first trade-off. USB 2.0 is specified for runs up to 5 m; USB 3.0 drops that to around 3 m because the faster signalling is more sensitive to line loss. Beyond those distances you need active cables or extenders, not just a longer jacket. Our catalogue spans 0.2 m patch leads through 2 m desk-length cables, which covers the vast majority of retail and OEM packaging.

Gauge and shielding matter next. Heavier conductors such as 22AWG keep voltage drop low on charging runs, and a 56k-ohm resistor on the data lines is what tells a legacy charger to behave. Foil or braided shielding is what separates a cable that works beside a motor from one that drops the connection every few minutes. If your end market is industrial, these are the lines to check first.

How to tell the versions apart on a sample

When a sample lands on your desk, there are three quick checks. Count the contacts: USB 2.0 Micro has five pins, USB 3.0 Micro-B has one extra row. Look for the blue insert or the SS marking on USB 3.0 hardware. And for Type-C, read the specification rather than trusting the connector shape. Any supplier who cannot answer these three questions in one email is guessing about their own product.

Quick checklist before ordering

Match the version to the slowest device on the bus, not to the newest one. Decide the length before the gauge, because length caps what gauge can rescue. Specify shielding when the environment is electrically noisy. And if your application sits between two versions, ask for samples of both rather than splitting the order on a guess. For anything that needs a non-standard length, connector or overmould, our custom cable service can build to drawing, and our factory page explains how production and inspection are run.

The full USB cable catalogue and charger cable range are organised by version, so you can shortlist by signalling rate before you compare prices.

Read more...
ISO 9001 quality systemCE · FCC · RoHS · REACH compliantOwn factory, 3,000 m² · 200+ staffExport to 110+ countriesReply within 24 hours